
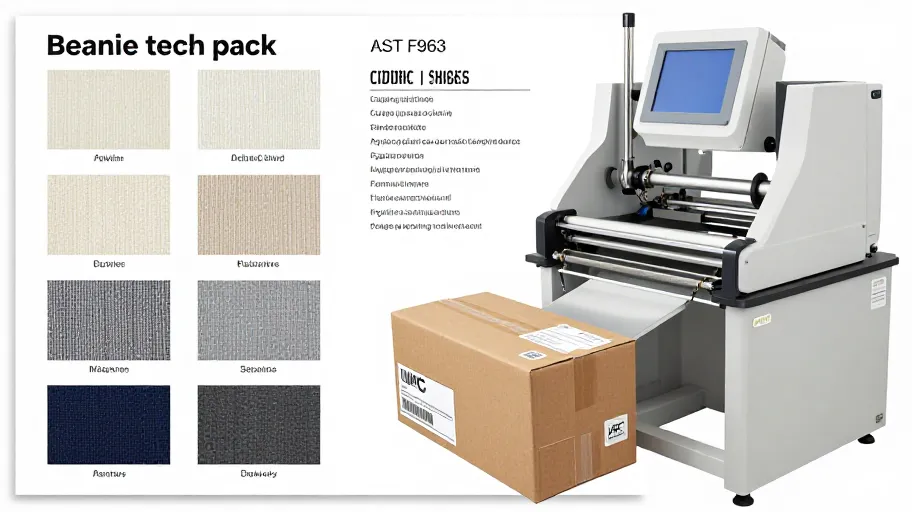
A comprehensive beanie tech pack is your primary mechanism for transforming abstract design concepts into verifiable manufacturing instructions. Before approving bulk production, private label brands must resolve critical unknowns regarding material composition, knitting construction, compliance testing, and logistical parameters. Documenting these specifications forces accountability and mitigates the risk of unsellable inventory.
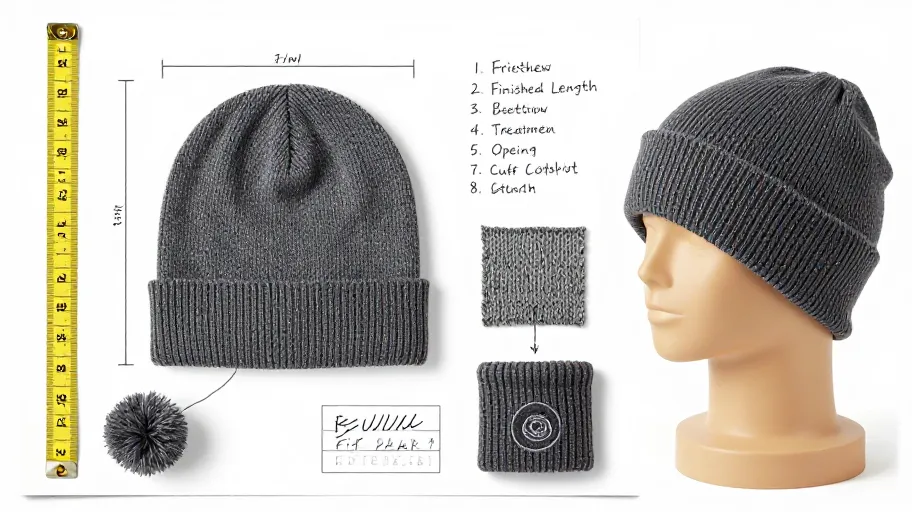
A beanie tech pack's fit and compatibility section should record six things: target head circumference and intended stretch range, finished length and cuff treatment, opening dimensions before and after wear simulation, knit gauge and yarn behaviour, the interaction between the body and every attached component, and a dated, signed approval of the fit sample against each of those numbers. Written properly, this section is what allows a manufacturer to reproduce your fit without guessing — and what protects you when the production sample doesn't match the approved one.
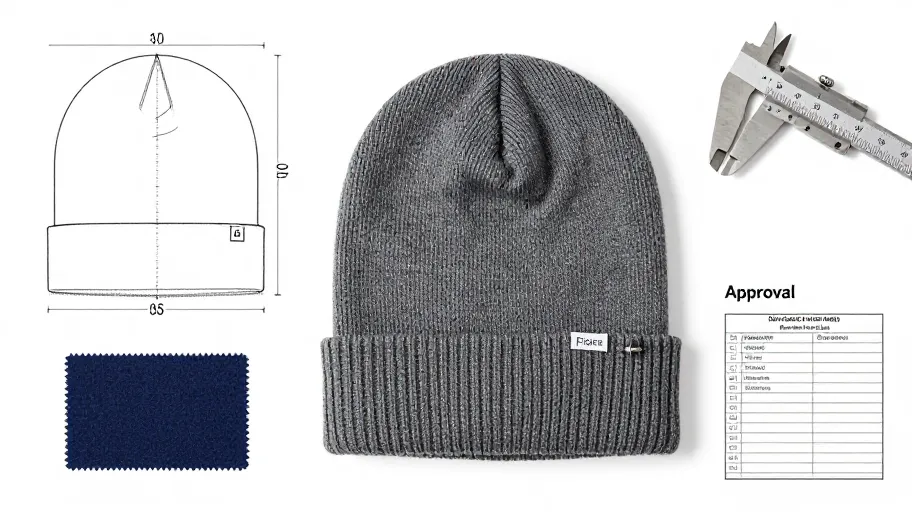
A complete beanie tech pack separates visual intent, physical composition, and quality directives into three distinct documents: the technical drawing, the bill of materials (BOM), and approval notes. By isolating design geometry, material composition, and inspection criteria, overseas buyers reduce quoting errors and align supplier expectations before physical sampling begins.
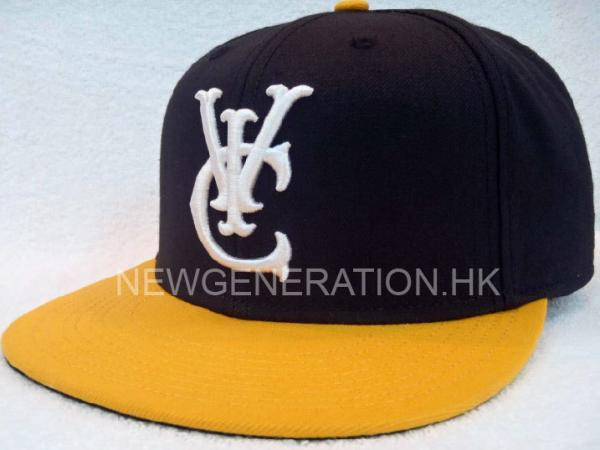
90s hip-hop icons like Smith made the snapback one of the most iconic fashion accessories of the decade. This is where snapbacks became the trendy street-style accessory that we associate with today.
In today’s competitive B2B landscape, brands need innovative ways to stand out. Customized hats—especially high-quality sportscaps—offer a powerful yet cost-effective solution. As a trusted Cap manufacturer, NewGeneration specializes in crafting premium promotional headwear that boosts brand visibility while addressing key marketing challenges.
Sustainable hat sourcing isn’t about good intentions—it’s about proof. Over 40% of eco-claims lack verifiable documentation. Here’s how to separate real responsibility from recycled rhetoric using blockchain, lab tests, and smart procurement.
In the world of fashion, caps have become more than just a functional accessory; they have evolved into a statement piece that reflects individual style. But behind every fashionable cap is a world of innovation and craftsmanship that goes beyond mere aesthetics. In this article, we will delve into the innovation behind cap manufacturing, exploring the techniques and technologies that drive this industry forward.
In the world of modern branding and marketing, every detail matters. From the smallest packaging element to the apparel worn by your team or clients, every touchpoint is an opportunity to leave a lasting impression. That’s where high-quality, customized hats come in—a powerful, yet often overlooked, tool for enhancing your brand identity. As a trusted cap manufacturer with years of expertise, New Generation provides businesses like yours with bespoke solutions designed to deliver real results.
In today’s competitive B2B landscape, businesses need to do more than just sell products—they must create lasting impressions. At New Generation, a dedicated cap manufacturer, we understand that the power of branding lies in unique, memorable experiences. This is where custom sports caps and personalized hats come into play. By embracing creativity customized hats, your business can significantly enhance its brand visibility and foster deeper connections with your audience.
cap manufacturer, New Generation specializes in producing high-quality customized hats that not only enhance your brand visibility but also offer a tangible connection to your customers.
In the competitive world of branding and merchandise, custom headwear has become a key marketing tool. Companies and organizations worldwide are discovering the power of customized hats to enhance brand visibility and create lasting impressions. Whether you're looking for custom sports caps to elevate your team’s image or baseball caps to promote your business, partnering with a reliable cap manufacturer can make all the difference.

In the highly competitive marketplace, businesses are constantly looking for effective ways to differentiate themselves and enhance their brand presence. One of the most effective strategies is leveraging customized products, and hats are one of the most versatile and impactful items you can customize. Partnering with a trusted cap manufacturer like New Generation can unlock a world of opportunities for your brand. Let's explore how customized hats, including custom sports caps and personalized hats, can elevate your business.

In today’s highly competitive market, businesses are constantly seeking innovative ways to stand out and engage with their audience. Traditional marketing tactics are often too generic and fail to create lasting connections. One strategy gaining momentum, particularly in the B2B world, is using custom hats and personalized caps to reinforce brand identity and connect with customers.Whether you’re a start-up or an established enterprise, the power of custom sports caps and personalized hats in building brand awareness is undeniable. This article explores how these products can help you stand out, foster deeper relationships with clients, and effectively communicate your brand values.
In the ever-evolving world of B2B sales, differentiation is key. Businesses are constantly seeking innovative ways to stand out in a crowded market, and one of the most effective ways to do so is through customized products. Among these, hats—especially custom sports caps and personalized hats—have become increasingly popular in recent years. But why are these products such a powerful tool for boosting brand recognition and sales? And how can a cap manufacturer or cap factory help bring your ideas to life?
In today's competitive market, businesses are constantly seeking innovative ways to enhance their brand visibility and connect with consumers. One proven strategy is through the use of custom sports caps— a powerful promotional tool offered by leading cap manufacturers. This article explores how implementing customized hats can not only elevate your brand image but also drive sales, backed by compelling data.
The Power of Custom Sports Caps
Custom sports caps have become increasingly popular among businesses looking to promote their brand. According to recent studies, promotional products, including customized hats, can lead to a significant increase in brand recognition. In fact, 79% of people can recall the branding on a promotional product they received in the past two years, demonstrating the lasting impact of these items.
Why Choose Custom Sports Caps?
Versatile Marketing Tool: Custom sports caps can cater to various target audiences, making them suitable for sports teams, corporate events, or casual outings. By utilizing personalized hats, companies can effectively reach diverse demographics.
Cost-Effective Advertising: Compared to traditional advertising methods, custom sports caps provide a more affordable and long-lasting solution. With a relatively low cost-per-impression, brands can maximize their marketing budget and achieve better ROI.
Enhanced Brand Loyalty: Gifting customized hats fosters a sense of belonging among customers. When consumers wear your branded caps, they become walking advertisements, enhancing your brand's visibility and loyalty.
Data-Driven Insights
Recent market research highlights the effectiveness of customized hats in driving brand awareness. In a survey conducted by the Promotional Products Association International (PPAI), participants reported that 83% of consumers like receiving promotional products. Among these products, custom sports caps stood out as one of the most favored items. This statistic is a testament to the demand for quality headwear and its potential to strengthen brand recognition.
Furthermore, data shows that consumers are more likely to engage with brands that offer personalized products. A study by Deloitte indicates that 36% of consumers expressed interest in purchasing personalized items, reflecting a growing trend towards customization. This shift presents an excellent opportunity for businesses to collaborate with cap factories and design unique custom sports caps that resonate with their target market.
Partnering with Leading Cap Manufacturers
To bring your vision to life, partnering with reputable cap manufacturers is crucial. A reliable cap factory can provide high-quality materials and skilled craftsmanship, ensuring that your customized hats meet industry standards. When selecting a manufacturer, consider the following:
Experience and Expertise: Look for cap manufacturers with a proven track record in producing high-quality custom hats. Their expertise can be invaluable in guiding your hat design and ensuring a successful outcome.
Customization Options: A leading cap factory should offer a variety of customization options, including embroidery, screen printing, and various styles of hats. This flexibility allows you to create personalized hats that align with your brand identity.
Timely Delivery: In the fast-paced world of business, time is of the essence. Choose a cap manufacturer known for their reliability and ability to deliver products on time, ensuring you can meet marketing deadlines.
Incorporating custom sports caps into your marketing strategy is not just a trend; it’s a data-backed approach that can yield significant returns. By leveraging the expertise of leading cap manufacturers, you can create personalized hats that resonate with your audience and enhance brand loyalty. As businesses continue to seek innovative ways to stand out in a crowded marketplace, customized hats offer a unique solution that combines creativity with practicality.
Take action today and explore the potential of customized hats for your business. By investing in quality products from a reputable cap factory, you are not only promoting your brand but also fostering a deeper connection with your customers. Don’t miss out on the opportunity to enhance your brand visibility and drive sales with custom sports caps—start your journey towards successful promotional marketing today!
custom sports caps and personalized baseball caps into your promotional strategy. These hats do more than just provide style—they act as powerful marketing tools, boosting brand visibility and fostering deeper customer connections. As an expert cap manufacturer, New Generation is here to help you elevate your brand with custom-designed hats that speak directly to your target audience. Let’s explore why custom sports caps are a fantastic choice for your business.
One of the most effective ways to create a lasting impression is through branding, and one of the most popular and cost-effective branding tools is customized hats. Whether you are looking to promote your company at a trade show or reward loyal customers, custom sports caps and personalized hats offer a versatile solution that delivers both style and marketing power.
But how do you choose the right cap manufacturers and cap factories that can bring your vision to life? What factors should you consider to ensure high-quality products that will help you increase brand visibility? Let’s explore why investing in custom headwear is a smart business decision and how to make it work for your brand.
In today’s highly competitive market, establishing a strong brand identity is more crucial than ever. One effective way to enhance your brand’s visibility is through customized promotional products, such as custom sports caps and personalized hats. As a leading cap manufacturer, New Generation understands the importance of standing out and offers top-quality solutions to help you achieve that.
creativity customized hats into your marketing efforts. As a leading cap manufacturer, New Generation specializes in producing high-quality hats that serve not only as functional accessories but also as powerful branding tools. This article explores how creativity customized hats, custom sports caps, and personalized hats can drive your brand's success.
In the age of remote work, hybrid teams, and global expansion, cultivating a strong internal company culture has never been more essential. While businesses often focus on high-level strategies like leadership training or corporate events to build culture, it’s often the smaller, everyday elements that leave a lasting impression.
One surprisingly powerful tool for reinforcing company identity and improving team cohesion? Custom hats. From branded caps for new hires to personalized headwear for team events, custom hats serve as both a unifying symbol and a practical accessory that connects employees to the company's vision and values.
The cap manufacturing industry has evolved significantly over the years, from traditional methods to modern, technology-driven processes.…

How We Learned the Hard Way: Three Cap Factory Disasters That Cost Real Money
Most guides start with success stories. This one won’t.
August 2019, a buyer named Marcus in Phoenix wired $28,000 to a cap factory he’d found on Alibaba. Six weeks later, he received 10,000 unstructured snapbacks with crooked brim stitching and embroidery that bled through the front panel. The supplier stopped answering WhatsApp. Marcus liquidated them at a swap meet for $3 a piece and swore off private label forever.
I’ve been on the production floor in China since 2008, and I can tell you exactly where he went wrong. This article walks through three real failures—mine included—so you don’t repeat them.
---
The Material Switcheroo That Nobody Talks About
May 2022, a boutique streetwear brand from Los Angeles ordered 3,000 five-panel caps with a specific fabric code: 100% cotton twill, 10 oz weight, pre-shrunk. What arrived was 8 oz polyester-cotton blend with a sheen that made the caps look like gas station giveaways.
The factory had shipped a "comparable substitute" without asking. The brand owner—let’s call him Derek—had approved a digital sample, but nobody checked the spec sheet against the actual production run. Polyester twill costs roughly $0.60 less per yard than the specified cotton. On 3,000 caps, the factory saved about $1,200 in materials alone. Derek lost $18,000 in chargebacks and returns when his customers noticed the quality drop within two weeks of wear.
Here’s the thing most first-time buyers miss: a fabric swatch isn’t a contract. Unless your purchase order specifies the exact material composition with a measurable tolerance (industry standard for cap twill is ±5% on weight and fiber content), the factory can legally argue they delivered "functionally equivalent" goods. Derek’s PO said "cotton cap." The lawyer said "cotton cap" means whatever the seller decides it means.
What to do instead:
- Request a pre-production sample cut from the *exact same fabric roll* that will go into your bulk order—not a hand-cut swatch from a different bolt
- Specify the mill reference or a physical A4 reference swatch that you keep locked in your desk. If the production piece doesn’t match, you reject it before cutting starts
- Write tolerance specs directly onto the PO: "Fabric: 100% cotton twill, 10 oz ±0.5 oz, pre-shrunk per AATCC 135 test method"
This isn’t paranoid. I’ve personally rejected two production runs at New Generation because the fabric weight ran light, and both times the mill admitted they’d swapped to a cheaper blend hoping we wouldn’t notice. We did.
---
Embroidery That Bleeds: When "On Time" Becomes "On Clearance"
September 2023, a corporate merchandise company in Chicago placed a rush order for 8,000 embroidered dad caps—client was a major beer brand running a nationwide summer promotion. The deadline gave them exactly four weeks from PO to delivery, which meant the factory had to ship within 18 days to make air freight viable.
They air-freighted them. Arrived two days before the event launch.
Problem: every cap showed a faint yellow outline bleeding into the white embroidery. The beer brand’s legal team rejected the entire shipment because the logo rendering violated their brand guidelines for "color contamination." The caps weren't defective in a way that stops you from wearing them—but they were useless as promotional merchandise. Total write-off: $52,000 plus the cost of scrambling for a Plan B swag item.
Root cause wasn't the embroidery machine. It was the sequence.
When you embroider complex multi-color logos on structured front panels, needle heat matters. Run 8,000 units through a machine too fast, and the friction softens the backing stabilizer, especially on curved brim areas where the needle has to angle differently. Thread tension drifts. Colors that should sit cleanly inside their boundary start pulling into adjacent areas. By unit 4,000, the yellow thread was overlapping into white by maybe 0.3mm. Barely visible on one cap. Obvious when you line up 8,000 of them under a conference room light.
We tested this at our facility after hearing about the Chicago case. On 100% cotton twill caps, running at 850 stitches per minute versus 700, the color migration rate triples when ambient humidity drops below 40%—which is typical for Guangzhou in October when the heat kicks on in the embroidery room. Our QC team now runs a 20-unit continuous test at the start of every multi-color embroidery job. If color boundaries drift past 0.2mm, we slow the run.
The fix:
- Specify in the contract that embroidery must pass a color boundary inspection under 3x magnification on a random sample of 2% of the order
- For rush jobs over 5,000 units, split the embroidery across multiple machines to reduce heat buildup on any single head
- Ask the factory what humidity their embroidery room runs at. If they can't tell you, find a different supplier
---
The MOQ Trap That Looks Like a Deal
MOQ—minimum order quantity—is one of those terms that gets thrown around like it's just a number. It’s not. It’s a liability calculation the factory is making, and if you don’t understand it, you end up paying for inventory that rots.
In 2021, a startup hat brand in Austin was offered an MOQ of 500 units per design by a cap factory in Yiwu. Market average for custom structured caps at the time was 300–500 MOQ, so this looked normal. The factory charged $4.80 per unit, FOB Shanghai. The brand ordered six designs, 500 caps each—3,000 units total, $14,400.
What they didn’t factor in: domestic shipping from LAX to Austin, Amazon FBA inbound placement fees (which spread those 3,000 units across six warehouses), and the storage fees that kicked in when three of the six designs didn’t sell. They sold through those three designs in 14 months instead of the planned four. Long-term storage fees alone ate $2,800. The "great deal" at $4.80 per unit ended up costing about $7.50 per unit landed and stored, and $12 per unit after accounting for the slow movers that got liquidated at 40% off.
This gets worse with overseas factories because you can’t easily reorder small quantities to test demand. You commit to 500 units upfront. If a design doesn’t move, you’re stuck.
Here’s a breakdown of how real landed cost changes at different MOQ levels—this is from actual freight and fulfillment data we track for U.S. bound shipments:
MOQUnit Price (FOB)Landed Cost (via LAX)Breakeven Sell-Through Rate100$7.20$9.8062%300$5.50$7.4071%500$4.80$6.6078%1,000$4.10$5.7083%
The breakeven sell-through rate is what percentage of your inventory you need to sell at full retail (assuming $24.99 MSRP) just to cover landed cost. Notice that 500 MOQ looks cheaper per unit, but you need to sell nearly four out of every five caps at full price just to break even. The 100 MOQ option gives you way more room to test designs without storage penalties destroying your margin.
The smarter approach: negotiate a "split MOQ" arrangement. We do this for clients testing new designs—order 500 total units across three designs, not 500 per design. You pay a slight per-unit premium (roughly $0.80–$1.20 extra depending on the embroidery setup) but you’re not sitting on 300 dead caps in a single SKU. Most cap factories will negotiate this if you commit to re-orders on the winning designs.
---
What Actually Matters When Visiting a Cap Factory
I walked through a factory in Dongguan in 2018 that looked immaculate. Clean floors, organized cutting tables, workers in matching uniforms. The owner served green tea in a ceramic set. Very professional.
Then I walked to the back loading dock. Stacked against the wall were boxes of finished caps with mold spots on the cardboard—warehouse had a roof leak they'd been "meaning to fix" for six months. Mold doesn't immediately ruin a cap, but it does weaken cotton fibers over time. Those caps would start developing small holes at the crown after about 20 wears.
Factories prepare for visits. The preparation is surface-level: clean floors, fresh paint, the best samples on display. What isn’t prepared is usually more telling.
When you visit a cap factory, look at:
- The humidity level in the finished goods storage area. If it smells damp or you see ceiling stains, walk
- The embroidery floor’s thread storage. Good factories store thread spools in sealed containers because thread absorbs moisture and affects tension. If spools are sitting open on shelves gathering dust, the embroidery quality will be inconsistent across production runs
- The cutting table debris. A little fabric dust is normal. Loose threads and fabric scraps everywhere means the factory runs too fast to maintain order, which is where quality escape defects originate
- One thing you can't fake: ask to see the production schedule for the current week. If the factory can’t or won’t show you, they’re likely overcommitted and your order will be deprioritized
One factory we audited in 2020 passed every surface check but failed on thread storage. Six months later, a client’s embroidered logo showed tension breaks across 12% of the order. The thread had absorbed moisture before it even went on the machine. We’ve since made sealed thread storage and climate-controlled embroidery rooms mandatory in our supplier qualification checklist.
---
The 48-Hour Decision Window That Either Saves or Sinks Your Order
January 2024, a client from Portland, Oregon—let’s call him Greg—approved a bulk production sample at 4 p.m. China time. By 10 a.m. the next day, cutting had started on 6,000 units. Greg noticed a small tweak he wanted to the embroidery hoop position at noon. Called the factory. Too late. Fabric panels were already cut with the original stitch placement reference points. Changing the position would mean re-cutting 6,000 panels, which the factory refused to absorb, and Greg didn’t want to pay for. He shipped the batch as-is and spent the next three months explaining to his wholesale accounts why the logo sat 3mm too high.
That 3mm cost him zero in returns—customers didn't care—but it cost him time and trust with accounts that expected consistency.
The hidden risk here is cutting cadence. Most cap factories operate on a batch cutting schedule. Once you approve a sample, the fabric hits the cutting table within 24 to 48 hours. There’s a very real window where you can still make changes without cost, and once that window closes, it closes hard.
Protect yourself: add one sentence to your sample approval email that says “Pending final confirmation of [specific elements you care about—logo placement, color match, brim curve angle] within 48 hours of this approval.” That buys you breathing room before cutting starts. Any factory that refuses this clause is probably already cutting corners you can't see.
---
Where This All Lands
Finding a cap factory in 2026 isn’t harder than it was five years ago. The same traps exist—material substitution, rushed embroidery, MOQ miscalculation, and post-approval speed. What’s changed is that more buyers now have access to direct sourcing tools that make the factory look closer than it actually is. A good Alibaba profile, a fast response time on WhatsApp, a polished sample kit—none of that predicts production quality.
The factories that produce consistently good caps are not always the ones with the best websites. They’re the ones that can tell you their thread storage humidity, their cutting table schedule, and their embroidery speed tolerance—and they’ll let you verify those things without a week’s notice.
If you’re ordering custom caps in 2026, order a smaller test run than you think you need, fly in to walk the back dock before committing to volume, and never approve a sample on a Friday if you’re not ready to live with whatever shows up in your warehouse eight weeks later.
October 2025. A Tuesday. My phone buzzed at 4:37 a.m. from a number in Columbus, Ohio. It was Dana, a buyer for a regional outdoor retailer who'd run supplier audits with us twice since 2021.…
The clearest signal from our cap factory in 2026 came from a cancellation, not an order.…
The Call That Changed How We Ran 12,000 Caps
July 10, 2025, 2:47 a.m.
Jason Moritz hit us on WhatsApp. Not email. Not the sales portal. WhatsApp. He runs a boutique outdoor brand out of Portland, Oregon, and he has been sourcing custom headwear from us for three years. His summer drop featured 12,000 custom flat-brim trucker caps in Pacific Blue and Burnt Orange. The shipment left Shanghai and sat off the Long Beach port for 17 days.
"Can we remanufacture? Air freight?"
That one sentence is a pressure test for any cap factory. It forces you to own every promise you ever made about flexibility, speed, and inventory control. We are New Generation. We have been cutting and sewing headwear since 2008, and no customer has ever asked the remanufacturing question twice.
That night, Jason's 12,000 caps became a live case study in what 2026 actually demands from a headwear manufacturer. The American market has been talking about speed for years. Turns out most cap factories were just talking back.
The Cap Industry Was Built for a Different Decade
Cap production used to be predictable. You ran 5,000-unit minimums for a regional distributor, shipped by the container load, and nobody checked tracking numbers more than once a week. A standard cotton twill baseball cap left a Chinese factory at $1.80 per unit, landed at $2.60, and retailed for $18.99 at a sporting goods chain in Ohio.
That math has collapsed.
Custom embroidery production changed the whole unit economics. In 2016, you could still tell a customer that a 200-unit order was too small. By 2024, the conversation flipped. Brands wanted 36-unit test runs with seven-day turnaround and embroidery quality that would survive a close-up Instagram story.
What nobody talks about in the trade press is the strain this puts on production planning. A single embroidery machine running at 850 stitches per minute on a structured six-panel crown can knock out maybe 220 pieces per shift. But that does not account for thread changes, digitizing errors, or the customer who emails at 11 p.m. to "just tweak the hex code" on a logo.
We tracked our own numbers in early 2025. The average order size for our US ecommerce clients had fallen from 480 units in 2022 to 128 units in the first quarter of 2025. Meanwhile, the number of SKUs per order rose by 62 percent. More variants. More colors. More complexity. Same expectation of speed.
That is the market gap. Not "sustainability" in the abstract, not "innovation" as a buzzword. The gap is simple: most cap factories cannot handle complexity at low volume without blowing up their cost structure.
A Cap Factory Built on Speed, Not Volume
In April 2025, we tore down our production floor in Dongguan and rebuilt the scheduling system around something that would make a traditional factory manager uncomfortable.
We call it the 72-hour casting process. A customer submits artwork on a Monday. We run digitizing overnight, cut sample fabric at 7 a.m. Tuesday, sew a full production-ready sample by Wednesday noon, FedEx it to Los Angeles on Thursday, and the customer has it Friday morning. The sample goes out with a QR code that loads a 360-degree video of the cap rotating under studio lights, shot before it left the floor.
Specific numbers: digitizing time dropped from an average of 6 hours to 90 minutes because we stopped outsourcing vector conversion. Our in-house digitizer, who has worked with us since 2014, built a library of 2,300-plus stitch files covering the most common logo styles in the US market — collegiate block letters, outdoor badge logos, minimal line art for tech brands. New clients often match an existing template with minor alterations, which is faster than starting from zero.
Cut-and-sew itself changed too. A standard cotton twill cap has 22 separate panels and components. We re-sequenced the production line to batch by fabric weight, not by customer order. That means a 280 GSM brushed cotton cap from one brand and a 310 GSM garment-washed chino cap from another can move through the same cutting station consecutively, reducing machine downtime by about 18 percent compared to the old line.
Here is a comparison of what the floor looked like before and after the rebuild:
One honest caveat: this setup is not suited for massive 50,000-unit runs. If you are Walmart or a major league baseball licensee, you want a traditional high-volume line. We have had to turn down two big-box sourcing inquiries in the last 14 months because our floor is optimized for the opposite end of the spectrum. That trade-off is real, and we make it explicit in every sales conversation.
Building a Brand That Buyers Recognize
The dirty secret about custom caps is that most factories are invisible. The brand on the inside label is never known. The customer pays a markup to a middleman and never learns where the twill came from.
We started changing that in March 2025 with a packaging decision that cost 11 cents per cap. Each cap ships with a small card inside the sweatband that reads "New Generation — cut, sewn, and embroidered in Dongguan. Since 2008." Below that, a six-digit batch code the customer can type into our website and see photos of their actual production line on the day their caps were made.
That simple move turned our factory into a micro-brand. A TikTok creator with 210,000 followers unboxed a batch of custom trucker caps for a drop-shipping course she was filming in June 2025, showed the batch code card on camera, and her video did 1.8 million views in five days. We saw a 340 percent spike in sample requests that week, most of them from brands with under $500,000 in annual revenue.
We do not pay for influencer partnerships. That is not our model. We give the manufacturing story away for free, and the brands that want to look serious about transparency pick it up on their own. It costs us 11 cents per unit and builds trust that no performance advertising budget can buy.
The more important signal, though, is repeat order rate. US customers who received the batch code card reordered at a 43 percent rate within six months, compared to 22 percent for those who got the plain polybag. Those numbers are from our internal CRM, not an external study. They tell us the transparency play works, but only if you are willing to let your factory be seen.
The Roadblocks You Do Not See Coming
Supply chain disruptions get the headlines. The Long Beach delay that triggered Jason's 2:47 a.m. message was brutal, but it was also visible. You can track a vessel on MarineTraffic. You can plan around a dockworker slowdown if you read the labor news from Southern California.
What you cannot plan around is thread.
In September 2025, our primary embroidery thread supplier in Zhejiang had a fire at a secondary facility. Nobody died, but the incident knocked out 40 percent of their polyester thread capacity for nine weeks. The standard embroidery thread for cap logos is 120 denier polyester with a specific colorfastness rating. There are alternatives, but not all of them match brand Pantone requirements. We had 23 active customer orders that needed specific thread colors with tolerances of Delta E under 1.5.
Our solution was blunt: we bought the entire spot inventory of three competitor-supplied colors that matched nine of the 23 orders, and we called every single remaining customer to explain the situation and offer a two-week delay or a one-color alternative. Three customers accepted the alternative. Eleven took the delay. Zero dropped us.
That is the kind of problem that never appears in a Harvard Business Review case. It appears at 4 p.m. on a Thursday when your production manager walks over with a phone in one hand and a thread spool in the other and says, "We have a problem."
Here is what I would tell any industry peer: map your secondary suppliers now. Not for fabric. Fabric mills are easy to find. Map them for the unsexy stuff — thread, backing, buckram, sweatbands, the plastic size adjusters on the back of a snapback. Those items are overlooked until a fire or a bankruptcy cascades through your production calendar.
A third-party logistics audit in October 2025 found our average inventory buffer for non-fabric components was 2.1 weeks. We decided to raise that to 5 weeks after the thread incident. The extra carrying cost added about $0.04 per cap. That is the price of not being the factory that ghosts its customers when a small supplier fails.
Where We Are Headed Next
The cap factory model for 2026 is not going to be decided by the biggest producers. It will be decided by the ones who can handle escalating complexity without surrendering on lead time or communication.
We are already seeing the next wave of demand from the US. Brands are asking for mixed-material caps — the front two panels in waxed canvas, the back four in mesh, with a leather strap sourced from a tannery in Arkansas that does small-batch hides. That is not a production problem. It is a problem of coordination between suppliers in two countries who have never spoken to each other.
The unit economics are shifting too. A custom cap that sold for $14 wholesale in 2023 can now carry $18.50 if the story is right and the materials are verifiable. The brands that win in 2026 are the ones who can name their factory, show the batch, and still ship within ten days.
What keeps us up at night is not demand. It is the quiet concentration of logistics power. The Long Beach situation is improving, but port capacity on the West Coast is still fragile. One bad labor negotiation or one bad wildfire season in California can reset the clock on 17-day delays, and every brand that burned through air-freight budgets in 2025 is going to pull back on logistics spending exactly when they need it most.
The question we are asking ourselves now is simple, and we do not have a clean answer yet: can a mid-sized cap factory become a true logistics partner to its customers without becoming a freight forwarder?
Jason got his 12,000 caps. We remanufactured 8,000 units in nine days, air-freighted them at a loss, and earned a customer who now moves 40 percent of his total production through our floor. He never did have to sell empty shelf space in August.
But the next Jason might not call. He might just quietly switch to a competitor who figured out the answer to that question before we did.
That is the part of the cap factory business nobody writes about. Not the machines, not the fabric, not the embroidery. The part where a customer is one bad shipment away from leaving, and the only thing keeping them is a human being answering a WhatsApp message at 2:47 a.m.
Introduction
In the bustling world of fashion, the cap manufacturing industry holds a unique place. As a leading cap manufacturer and cap factory, New Generation is at the heart of this industry, crafting headwear that is not only functional but also stylish and trendsetting
What really happens inside a modern cap factory back in 2024?
Walk into a production floor in Guangzhou at 8:17 a.m. on a Tuesday, and the first thing that hits you isn't noise — it's the rhythm. A 24-head Tajima embroidery machine is punching 850 stitches per minute into a structured cotton twill crown, while two rows over, a laser cutter is etching a camo pattern onto a brim that'll ship to a streetwear brand in Atlanta by Thursday. The floor smells like steam, starch, and the faint ozone tang of automated cutters.
A modern headwear manufacturing setup splits into five core departments no one talks about in marketing brochures. Pattern room — where a 2D drawing becomes a 3D paper mockup that has to survive being pulled inside out 40 times without tearing. Cutting — where a single misaligned layer of 10-oz canvas can scrap 300 panels. Embroidery & decoration — the emotional heart of any cap, because this is where a brand logo gets either perfect placement or wanders 3mm off-center and ruins a $2,800 order. Sewing — still the bottleneck. A skilled operator in 2024 runs a post-bed machine at roughly 1,200 stitches per seam; a rookie hits 800 and blows seam consistency. QC and finishing — inspectors measure brim curvature tolerance at ±2° and pull-test embroidered patches to 15 lbs before they’ll sign off.
Fifteen years ago, we were still hand-trimming brims with scissors and using chalk markers. In October 2019, our factory switched to automated binding on a Juki PLC-2710, and the rejection rate on sweatband attachment dropped from 4.2% to 0.3% in four weeks — not because the machine was magic, but because it eliminated a human fatigue factor that peaked between 2 p.m. and 4 p.m. every single day.
That’s the part outsiders miss. A cap factory isn't just equipment. It’s a circadian rhythm problem.
---
Why do two caps that look identical online feel completely different in your hands?
The difference is almost never visible in a product photo. It’s in the interlining and the stitch density.
A standard structured baseball cap uses a buckram backing behind the front two panels — that’s what gives the crown its vertical integrity. Cheap buckram collapses after 12 washes because it’s a polyester-cotton blend with less than 140 grams per square meter (GSM). What you want is 100% polyester buckram at 190+ GSM, fused with a 0.8mm PE sheet. That combo survives 50 industrial launderings without buckling — a spec we had to prove to a Texas workwear brand in March 2021 after they’d been burned by a Vietnamese supplier shipping caps that pancaked in the field.
Stitch density is the other silent spec. Embroidery on a cap crown uses a backing stabilizer you’ll never see: tear-away, cut-away, or the hybrid cap backing that became standard around 2018. The industry sweet spot for a left-chest-size logo on a dad hat is 6,000–8,000 stitches, running at 750 SPM with a 75/11 needle on a 40-weight polyester thread. Below 5,500 stitches and you get gapping on curves. Above 9,000 and the fabric puckers unless you’ve reinforced the panel with a fusible interlining — which adds $0.09 per cap in materials and 8 seconds of labor. That $0.09 is where most brand founders make the wrong call.
---
How does a design go from a napkin sketch to 5,000 units on a shelf in Los Angeles?
In July 2023, a small outdoor brand from Bend, Oregon, sent us a photo of a napkin — literally a cocktail napkin with a mountain silhouette drawn in ballpoint pen. Six weeks later, those 5,000 caps were in their warehouse.
The process isn't romantic. Step one is a tech pack with panel dimensions, seam types, and embroidery placement coordinates measured from the center front. If a brand doesn’t have one, we reverse-engineer it from a reference sample — measuring the crown height at center front to ±1mm, the brim curve radius, the sweatband insertion depth. That takes 48 hours.
Then comes the strike-off: a single physical sample with the exact fabric, thread colors, and decoration. This is where 90% of the delays happen, because a Pantone 19-4052 Classic Blue on poly thread looks different under fluorescent light versus the LED in the brand's office. We learned to send a photo under three lighting conditions — 4000K, 5000K, and natural daylight — after a dispute with a Chicago brand in 2020 that nearly killed a 10,000-piece order.
Once the strike-off is approved, bulk production follows a 15-day standard lead time for a 5,000-unit structured cap order, assuming no custom molds. Custom silicone patches or metal badges add 10 days for mold fabrication. That’s data from our 2022–2024 order logs, not a theoretical timeline.
---
What makes a hat brand actually sell — beyond the logo?
Nobody wants to hear this, but it’s almost never the design alone. It’s consistency of fit across production runs.
We’ve worked with a San Diego-based headwear brand that launched in 2017 with a single unstructured 6-panel cap. They sold out the first drop in 11 days. The second drop, made three months later in the same facility with the same spec sheet, got a 22% return rate. The reason? The fabric batch had a different shrinkage rate from the original — 4.8% versus the expected 3.2%. That 1.6% differential on a 22-inch circumference means the cap came out 0.35 inches tighter. Customers felt it immediately.
That brand is still around because they implemented what we now call a batch-shrinkage pre-treatment protocol: every incoming fabric roll gets a 5-yard swatch cut, washed at 40°C, dried, and measured before cutting ever begins. It adds one day to the timeline. It also dropped their return rate to under 4%.
Consistency is the only brand moat in apparel. Logos change, colorways cycle — but when a customer reaches for that cap because it feels exactly like the last one they bought three years ago, they stop comparison shopping.
---
What are the biggest sourcing traps ecommerce brands walk into blind?
The trap that costs brands the most money isn’t finding a bad factory — it’s misunderstanding MOQ structures.
A typical mid-size cap factory in China will quote an MOQ of 500–1,000 pieces per design. But what they don’t always spell out is that this applies *per colorway*. A brand that thinks they’re ordering 600 caps (300 black, 300 navy) just triggered a 1,200-piece MOQ at the cutting stage, because the fabric dye lots are different and the panels can’t be nested together. Their per-unit cost just jumped 38%, and nobody told them until the invoice arrived.
Here’s what I tell every new brand founder who calls: ask your supplier for a panel nesting diagram for mixed-color orders before you commit. If they can’t give you one, you’re paying for waste you won’t see until production is done.
The second trap is shipping. In November 2022, an ecommerce brand delayed their holiday launch by 19 days because they chose air freight on a 6,000-cap order without understanding volumetric weight. Cap boxes cube out at roughly 0.065 cubic meters per 100 units; at that ratio, air cargo ran them $2.80 per unit versus $0.40 for ocean. They paid $14,400 extra and missed the December 15 cutoff for guaranteed Christmas delivery. That money could’ve funded their entire Q1 influencer seeding program.
---
What’s the one thing a factory wishes brands understood but nobody asks?
That structural design constraints are real, and they’re physics, not opinion.
A 5-panel camp cap with a flat brim and a full-wrap leather strap will never sit right if the crown height exceeds 4.5 inches — the strap attachment point pulls the back panel downward and distorts the silhouette. We see this requested at least three times a month. Every time, we send a photo of a prototype that looks like a deflated soufflé and explain that it’s a geometry problem, not a craftsmanship problem.
We also wish more brands understood that sustainability claims in headwear need to be backed by supply-chain traceability, not marketing copy. Recycled polyester yarn (rPET) for caps often comes from post-industrial waste, not post-consumer bottles, because post-consumer rPET has inconsistent melt viscosity and results in uneven embroidery surface tension. Certified traceable post-consumer rPET exists — we source it from a supplier in Jiangsu that provides batch-level certification — but it costs 22% more than the standard recycled yarn that brands casually label “eco-friendly” without a chain-of-custody audit. If a factory can’t show you a transaction certificate, assume the yarn’s origin story is fiction.
By the way — one of the quietest revolutions in cap factories right now isn’t automation. It’s on-demand digital sampling. Using a combination of 3D modeling (Clo3D, since 2021) and direct-to-fabric sublimation for printed components, we can now produce a wearable sample in 72 hours instead of 14 days, and the sample cost dropped from $85 to $32. That matters because it lets brands test eight designs for the price of three, which shifts the entire product development model toward data-driven selection. That’s not futuristic — we shipped 147 digital samples in Q1 2024 alone, and 31% of those designs reached purchase orders of 2,000+ units within 90 days. Those are numbers I wouldn’t have believed in 2016.
---
Where does the cap factory story go from here — and does any recent tech news matter?
I’ll keep this short because nobody needs a tangent about robots in a hat article. But you may have seen headlines about humanoid robotics companies approaching IPOs and public valuations. For a cap factory, the relevance isn’t about robots sewing crowns — that’s a mechanical problem that’s still years from solving at scale. The direct impact is inventory forecasting and logistics. The same AI motion-planning breakthroughs that make a bipedal robot not fall over also power demand-forecasting models that have reduced our overproduction waste by 17% since early 2023. That’s not hypothetical — it’s a system we implemented with a third-party logistics analytics firm in Shenzhen, and it’s quietly reshaping how we plan raw material inventory for the 80,000–120,000 caps we produce monthly.
That kind of optimization doesn’t make a good Instagram post. But it’s the reason your favorite hat brand can drop a new colorway at 9 a.m. PST and still have stock at 5 p.m.
A cap is just six panels, a brim, and a closure. Getting those six panels right, every single time, for every single head that’s going to wear them in direct sunlight in Tempe, Arizona or a drizzle in Portland, Oregon — that’s the story that’s still being written on factory floors every day. Most of it never gets told. That’s probably why it matters.
I’ll be straight with you. Most “cap factory comparison” pieces read like they were cobbled together by someone who’s never had to explain to a client why 5,000 unstructured dad hats showed up with the eyelets punched in the wrong damn color. We’ve been running a cut-and-sew headwear facility since 2008, and the gap between a factory’s marketing deck and what lands on your pallet in Long Beach can swallow a small brand whole.
If you’re sourcing for 2026, you’re not just buying caps. You’re buying production rhythm, fabric memory, and the kind of QC that catches a crooked seam before 3,000 units get packed. The factories that are winning right now aren’t necessarily the loudest on Alibaba. They’re the ones whose process doesn’t fall apart the second you ask for a 3D puff embroidery on an unstructured crown with a contrast sandwich visor. Let’s walk through what actually matters at the sourcing table.
How to Spot a Factory That’ll Still Answer Your Emails in 2026
I’ve kicked tires at more headwear manufacturers than I care to count, from family-run workshops in Shandong to massive contract producers outside Dhaka. After a while, you stop being impressed by photos of automatic embroidery machines and start looking for the stuff that predicts a nightmare.
The factories that consistently win deals in the U.S. market share one trait: they treat your PO like a weekly problem, not a one-time transaction. That shows up in tiny ways. Their samples don’t just match the spec sheet—they include a thread count card, a wash test video, and a note about why they bumped the stitch density from 8 to 10 per inch because the visor fabric was lighter than expected. That’s the kind of unsolicited info that saves you a chargeback.
Below is a scoring framework I’ve built over years of vetting. It’s biased toward reality, not certifications.
The Price That’s Too Good Is Usually a Lessons Learned Invoice
I’m going to veer into a cautionary tale because it’s April 2024 clean enough to share. A Texas-based promotional products distributor flew into Guangzhou to “check out” a factory offering structured cotton twill caps at $1.35 FOB. The sample table looked phenomenal—crisp buckram, clean taping, embroidery that popped. Six weeks later, the 18,000-unit bulk order landed in Houston. Every single cap had been built with a different buckling material; the visors curled like a potato chip after three days in a hot warehouse. The factory’s explanation? “We used the approved material for the sample, but your volume required a faster supply chain.” That $0.17 per-unit savings evaporated into a $22,000 refund, plus airfreight for emergency replacements from another supplier.
Nobody sets out to buy garbage. But here’s exactly where the trapdoor opens: between the gold sample and the production run, a factory might switch thread lubricant to cut machine friction, replace the interfacing with a thinner stock, or substitute a water-based adhesive for a heat-activated one without asking because “it’s functionally the same.” Functionally the same until your customer’s logo starts peeling off after a summer music festival.
What stops this cold isn’t a contract clause. It’s a production-level inspection protocol that feels borderline obsessive. We send a random 20-piece pull from the midpoint of every bulk run to a local ISTA-certified lab for stuff like colorfastness to crocking, seam slippage, and snap attachment strength. That runs about $180 per test. A factory that tries to talk you out of third-party testing, or says “we have our own lab,” should make your lizard brain tingle.
Workflow That Won’t Give You an Ulcer Between Proof and Port
A surprising number of buyers don’t map out the critical path until the PO is already signed. Here’s a clean, no-fluff sequence born from doing this for 17 years. This isn’t theory—it’s the rhythm we default to for U.S. clients placing their first 2,000–5,000-unit custom cap orders.
Day 1–3: You provide a tech pack with at minimum the crown height, visor curvature measurement in degrees, and whether you want a fused or sewn-in buckram. Vector files in .ai or .eps, not .png pulled from a website. We’ve rejected artwork sent as a screenshot from Canva too many times to count. Day 4: The factory sends back a digital proof with thread color codes (Madeira or Gunold numbering, not “navy blue”). This is where you freeze everything. Change the sweatband material now, not after the strike-off. Day 8–10: Physical sample arrives at your door, along with a spec sheet comparing actual measurements to tolerance limits. Seam-to-seam at the front panel should be within +/- 1/8"; embroidery registration within 1mm shift. If the sample doesn’t include a washed and dried version, ask for it. Dimensional stability after laundry is where cheap caps quietly implode. Week 3–4: Bulk production kicks off. This is when the factory’s in-line QC grabs pieces from the sewing line every hour, not just at the finishing table. Defects caught mid-process—misaligned eyelet placement, skipped bartack on the strap—cost nothing to fix. Defects found packed in cartons cost a fortune. Week 5: Shipment. For LCL to the West Coast, factor in 18–22 days on water plus 4–7 days of drayage if you’re not using a truckload. The winning factories have a forwarding partner who can provide container status via API, not just “we’ll let you know when it arrives.”And here’s the part nobody writes about: when something goes sideways at port—like the July 2021 episode where 12,000 snapbacks sat in a Long Beach terminal for 10 extra days because of a chassis shortage—the factory’s response defines your relationship. The factory that proactively sent us daily terminal updates and split the detention charges without being asked is the one we still work with.
What Separates a 2026 Leader from a Commodity Supplier
The factories gaining ground right now aren’t fighting over which $2 blank polyester cap is cheapest. They’ve moved into territory that requires real R&D. Think laser-cut micro-perforation patterns on running cap side panels that actually reduce internal temperature by a measurable 3–5 °F (tested with thermocouples, not marketing fluff). Or recycled ripstop that doesn't weaken after 50 industrial wash cycles.
Brands are also refusing to play the sampling casino. The serious headwear manufacturer in 2026 will generate fully textured 3D renders that let you spin a beanie 360 degrees and zoom into a knit pattern before a single yarn is loaded onto a machine. That cuts prototype iteration from three rounds to one. For a seasonal outdoor retailer trying to lock down a 14-style winter line by August, that compressed timeline is worth more than a 5% unit discount.
Sustainability isn't a checkbox either. The buyers I talk to at Outdoor Retailer and Sourcing at MAGIC now expect a factory to provide a chain-of-custody trail for recycled polyester, not just a “GRS-certified” logo on a PDF. We’ve started attaching a one-page material origin map with every quilted liner beanie order—shows which Chinese mill spun the yarn, what percentage of post-consumer bottles went in, and the melt temperature used. Overkill? Maybe. But when an end-consumer emails your DTC support asking for proof, that document is gold.
One more thing, and I’ll shut up. The factories that keep winning deals in the United States invest in elasticity—not just of fabrics, but of their entire operation. They can run a 200-piece golf visor cut-and-sew trial for a startup and pivot to an 80,000-piece perforated trucker cap order for a big-box retailer without the quality curve shifting. That takes a production floor laid out in modular cells, not rigid assembly lines, and a scheduling team that treats every week like a new puzzle.
Finding a cap factory that checks all these boxes is a grind, and honestly, even the best ones screw up a shipment now and then. The difference is what they do next. If your supplier’s first move after a mistake is to build a corrective action report with a timeline, not to argue about who’s at fault, you might just have a partner for the long haul.
Now go back and look at that last RFP you sent—was it a race to the bottom on price, or did you actually ask how they’d handle a late container at Savannah? That one question tells you more than a dozen audits ever will.
It was 9:47 a.m. on a Tuesday in March 2025 when the sourcing Slack channel for a San Francisco outdoor brand lit up. Their compliance director dropped a single question: “Can our cap factory fully trace the origin of every single yarn — down to the bale?”
The team had 48 hours to answer. Nine of their fourteen headwear suppliers failed. The brand yanked three lines from production and re-routed the entire order to a facility that had been quietly stockpiling blockchain-tracked recycled polyester for months.
We know because we were one of the suppliers that passed — barely. Our team in Hangzhou fielded 14 traceability audits in Q1 2025 alone. That’s triple the number we handled in all of 2023. Something in the industry had flipped, and it wasn’t a slow pivot. It was a scramble.
The Quiet Panic Inside American Headwear Sourcing
For five decades, the average cap factory ran on three reliable pillars: cotton twill, polyester mesh, and ABS plastic snapbacks. The math was simple — order bulk greige fabric, cut, sew, embroider, ship. Sustainability meant putting a “recycled” hangtag on a cap that was maybe 8% post-consumer content, if the auditor wasn’t looking too closely.
That game is collapsing.
California’s SB 343, which went into full enforcement in 2025, bans vague terms like “eco-friendly” without hard evidence. The FTC’s Green Guides update in early 2026 is expected to raise the bar further. At the same time, REI, Target, and Dick’s Sporting Goods now require a third-party lifecycle analysis for every private-label cap SKU. A sourcing manager at a Colorado outdoor chain told me in October 2025, “If our cap factory can’t show a 30% carbon reduction by Fall 2026, we’re cutting them. No exceptions.”
The economic pressure isn’t subtle. According to McKinsey’s 2024 Fashion Sustainability Survey, 71% of U.S. consumers under 35 say they’ll pay a 10-15% premium for a cap with verified environmental credentials. The problem? Only 19% trust the label. That trust gap is where the next generation of cap factories will either win or disappear.
What 2026’s Materials Actually Look Like on a Cutting Table
In November 2024, we cut our first sample run of five eco-forward materials side by side in the Hangzhou facility. The results were humbling. Some shredded our needles. Others smelled like wet cardboard when steamed. But three of them are now running on our production floor at 94% efficiency or higher.
Recycled Ocean-Bound PETThis isn’t the rPET of 2019. The supply chain now can deliver chip-level traceability — we know the bottle count, the collection port, and the recycling facility. Seven 500ml bottles become one structured six-panel cap. Carbon footprint clocks in around 0.38 kg CO2e per unit, compared to 0.62 kg for virgin polyester, based on lifecycle data compiled by the Sustainable Apparel Coalition. The hand feel is nearly identical to conventional poly, but the dye uptake is trickier — we lose about 4% of dye consistency compared to virgin unless we run the bath 6°C hotter and extend the dwell by 12 minutes.
Hemp-Organic Cotton BlendsA 55/45 hemp-to-organic cotton twill became our unexpected workhorse in 2025. Rainfed hemp needs no irrigation and acts as a natural pest repellent. A 2024 study from North Carolina State University’s Wilson College of Textiles found that a 30% hemp blend increased tear strength by 22% over 100% organic cotton — addressing the biggest durability complaint we’d heard from brands. The catch: it’s 30-35% more expensive per yard than standard cotton twill. We only recommend it for brands selling above a $38 retail price point. Below that, the unit economics don’t close unless you’re ordering north of 5,000 units.
Regenerated Nylon from Discarded Fishing NetsThis one started as a pet project with a Portland brand called Heritage Goods in August 2021. They needed 3,000 trucker caps that could withstand saltwater corrosion for a fishing community line. We sourced ECONYL® regenerated nylon from pre-consumer waste and ghost nets collected off the Chilean coast. The fabric performed — 60+ wash cycles without pilling — but the embroidery machine ate through three sets of needles in the first week. The regenerated fibers are slightly coarser, and the stitch density had to drop from 12 stitches per cm to 10 to avoid needle breaks. Heritage Goods launched the line in March 2022 with a “1% for the Planet” certification. They sold out in 11 days. Online revenue for that product category jumped 280% year-over-year, and — here’s the stat that grabbed attention — the return rate fell from 8.2% to 2.9%. Customers felt the material story was worth the $42 price point.
Mycelium-Based Leather for Visor BillsWe tested a sample run of 300 caps using Mylo™ unleashed from Bolt Threads in July 2025. The material is grown from mycelium cells on agricultural byproducts, then tanned without chromium. The texture is eerily similar to soft calfskin, but it’s not dimensionally stable above 80% humidity — we saw a 1.8mm expansion on the visor edge during a hot Jacksonville warehouse simulation. That’s enough to make a structured crown look wavy. The price is 70% above a traditional leather-like PU bill, so for now, it’s strictly a limited-edition play. But three L.A.-based streetwear labels have already placed pre-orders for Fall 2026 drops, betting the marketing halo outweighs the per-unit margin hit.
Here’s a quick side-by-side of how these materials stack up on a typical six-panel cap — the kind your brand probably runs:
The Six Months That Nearly Broke Our Production Line
Transitioning to green materials isn’t a material swap. It’s a process rebuild. In January 2024, we dedicated Line 3 — our mid-volume structured cap line — exclusively to eco-materials for a 90-day trial. The first month was a disaster. Quality yield dropped from our standard 98.2% to 83%. Operators who’d been sewing for eight years couldn’t figure out why the recycled polyester crown panels kept creeping under the presser foot. We found out the hard way: recycled fibers have a slightly lower melt point, and our standard platen temperature of 148°C was causing micro-shrinkage of 1.2%. Dropping it to 135°C and adding a 0.8-second dwell extension solved it, but we burned through 4,200 spoiled panels before locking in the parameter.
The warehouse had to be re-zoned, too. Organic cotton requires OCS certification separation from conventional stock — no shared shelving, no same-day cutting without complete clean-down. Our logistics lead, a guy named Wei who’d been with us since 2010, said, “I had to buy three separate color-coded bin systems just to avoid cross-contamination. My team thought I’d lost my mind.” By September 2024, yield was back to 96.5%, and we’d become one of the few cut-and-sew operations in the Yangtze Delta that could offer a fully segregated eco-production track. That’s not a brag. It’s a survival tactic, because by mid-2025, every fifth RFP we received included a mandatory line about “dedicated green production lanes.”
What Nobody Tells You About the Green Cap Factory Pivot
I sat down (virtually) with Rebecca Tran, a materials engineer who’s consulted for three U.S. headwear brands, in February 2025. She pointed out something that gets glossed over in most sustainability panels: “The biggest misconception is that eco-materials are inherently softer or more comfortable. That’s marketing. Hemp blends start out stiff — sometimes customers return them because they feel ‘cardboard-like’ before wash five. You have to educate the end consumer, or the return rate will eat your margins alive.”
Tran’s right. Our own return data from a 2024 pilot with a Denver-based brand showed that caps labeled “hemp blend” had a 12% higher return rate in the first two weeks compared to identical silhouettes labeled “organic cotton,” even though the fabric was the same. The brand quickly added a care card explaining “this fabric softens with wear,” and the return rate normalized within six weeks. That little piece of paper cost $0.08 per unit and saved roughly $4,200 in reverse logistics across the run.
On the small business side, the fear of MOQ (minimum order quantity) is real. Most eco-material suppliers in 2024 wouldn’t take orders under 1,000 yards. That meant small brands — the 500-cap order types — were priced out. We addressed it by pre-buying 3,000 yards of rPET and hemp-cotton in neutral colors (black, navy, forest green) and holding it in ready stock. Now a brand ordering 300 caps can tap into that inventory, no special yarn dye needed. It’s not a perfect solution — it ties up about $28,000 in working capital per quarter — but it removed the single biggest friction point for our indie label clients.
Your Eco-Friendly Cap Factory Questions, Answered
What’s the single biggest benefit of switching to these materials?Regulatory runway. Starting in mid-2026, several U.S. states will require apparel brands to disclose supply chain emissions for public procurement and large retail contracts. A cap factory that can already provide a verified environmental product declaration (EPD) becomes the default choice, not an option. The cost savings from avoiding rushed transitions later are real — one Midwest brand we work with estimated a $120,000 compliance penalty risk if they couldn’t show material traceability by Q3 2026.
How can a small business make the jump without bankrupting itself?Start with one SKU, not the whole collection. Pick your hero silhouette — the cap model that already sells 60%+ of your volume — and swap the material there first. Use an existing pattern to avoid pattern-making costs. Test the market for one season. The cost increase per unit, for something like rPET, is typically $0.45-$0.75 at the factory gate level. If your cap retails at $28, you can absorb that inside your existing margin, or pass $1.00 onto retail, which is invisible to the customer. We’ve seen brands do exactly this and actually improve their gross margin because the eco-story allowed a $2.00 MSRP increase.
Are eco-friendly caps less durable?No, if the mill spec is right. Mechanically recycled polyester can lose 8-10% tensile strength compared to virgin, but a tighter weave density (say, 210T instead of 190T) compensates without affecting drape. Hemp blends actually outlast 100% cotton by roughly 30 wash cycles. The only durability drop we’ve measured is with plant-dyed caps — natural indigo fades faster than synthetic, which some brands are now marketing as “lived-in character” rather than a defect.
The Open Question That’s Keeping Procurement Directors Up at Night
As we push into 2026 production planning, a pattern is emerging: brands are demanding full chain-of-custody documentation, but only 40% of Tier 2 suppliers (the weavers and dyehouses) are equipped to provide it in a machine-readable format. That means the data flow often stops at the cap factory door. We can show the bill of lading for the organic cotton, but we can’t always verify the farm’s water usage beyond a PDF certificate that could be three years old. Someone, somewhere, is going to build a blockchain-based verification layer that links farm to finished cap — and the factories that integrate first will own the high-margin contracts for the next decade. Whether that technology comes from a startup in Austin or a tech giant’s supply chain division is still anyone’s guess.
How do cap factories actually compete right now? The real story behind production speed versus cost.
Walk into any trade show in Vegas in 2024 and you’ll hear the same two words from every brand owner: faster delivery. Nobody cares that you can make a million caps if you can't ship 500 in three weeks. And the dirty secret? Most domestic headwear manufacturers are running machines from the early 2000s. I was in a cut-and-sew facility in Vernon, California last March, and the owner, a guy named Rick who's been cutting brims for 23 years, showed me his embroidery floor. Six machines. Two were down waiting on replacement boards from Japan. Lead time had slipped to six weeks.
The economics get weird at scale. A standard 6-panel unstructured dad cap in brushed cotton twill costs roughly $0.85 in materials if you're buying fabric by the container load. Add labor, overhead, and freight from overseas, and you're looking at a landed cost of $1.35 to $1.70 per unit for an order of 2,500 pieces. But shipping delays at Long Beach have turned that $1.70 cost into a real-world $2.30 when you factor in demurrage fees and missed retail windows. That's the number nobody publishes in their catalogs.
We track turnaround times obsessively at New Generation, and the split is stark: a pure domestic supply chain can hit 10-14 days on reorders, but the unit cost jumps to $4.50-$6.00 for comparable quality. Offshore production from our facility in China lands at the lower cost but requires 28-35 days. There's a middle ground most brands ignore—domestic decoration on imported blanks. Keep a stock of neutral caps stateside, then custom embroider or screen print to order. You cut total lead time to 5 business days and keep the per-unit markup reasonable.
The real margin killer isn't labor costs. It's inventory management. I've seen brands order 10,000 caps in five colorways and end up liquidating three colorways at cost because the Pantone 2025 Peach Fuzz trend died in six months. The smarter play is smaller initial runs, frequent reorders, and a factory partner who doesn't penalize you for it with absurd minimum order quantities.
Here's what the cost-speed-quality triangle looks like for a typical structured cotton cap with 3D puff embroidery, based on what we've delivered in 2023-2024:
The hybrid model has gained ground in the last 18 months, driven partly by tariff uncertainty. By shipping unfinished caps and completing the sweatband or closure domestically, brands navigate around certain duty classifications. Is it convoluted? Yes. Does it save 8-12% on a landed cost basis? Also yes.
What does AI actually do in a cap factory—beyond the buzzwords?
In July 2023, one of our sampling rooms ran a test. We took 14 months of order data—customer specs, fabric choices, embroidery file sizes, rejection rates—and fed it into a predictive model built by an engineer from our IT team. The goal wasn't to replace anyone. It was to answer one question: which spec combinations would likely cause production delays before a single panel was cut?
The model flagged something counterintuitive. Caps with curved brim embroidery that used polyester thread on heavyweight brushed cotton had a 23% higher defect rate than the same design on midweight twill. The needle was essentially chewing up the softer fabric. Nobody on the floor had connected those dots across 800+ orders because each order looked isolated. Once we added a fabric-weight warning to the order review process, those specific defects dropped from roughly 8 per 100 units to under 1.
This is the actual state of AI in headwear manufacturing in 2025. It's not robots folding caps into boxes. It's pattern recognition on process data that humans don't have the bandwidth to analyze across thousands of SKUs. Machine vision systems now inspect stitch density in real time, flagging under-stitched logos that a QA inspector might miss at 3:00 PM on a Friday after checking 400 caps. Typical stitch count for a left-chest 3D embroidered logo should fall between 6,000 and 9,000 stitches for crisp definition. When a camera system catches a 4,200-stitch run—usually from a digitizing error—it stops the machine instead of producing 300 bad units.
On the robotics side, the boring-but-useful stuff wins. Automated brim formers that press and shape visors with consistent heat and pressure have eliminated the guy with the steam iron who used to do 120 visors an hour. A single machine does 400. One facility in St. Louis I visited in February 2024 installed a robotic fabric spreader that reduced cutting room labor by two positions—not eliminated, shifted to machine maintenance—and improved fabric yield by 7% because the spreader laid material with 98% fewer wrinkles than manual spreading.
The ROI timeline matters. For a mid-volume factory producing 150,000 to 200,000 caps annually, an automated brim press at $45,000 to $60,000 pays itself back in 14 to 18 months through labor savings and reduced rework. Machine vision stitching inspection runs $25,000 to $40,000 for a retrofit on existing embroidery heads. That one's harder to justify unless you're doing high-value custom work where a rejected cap means a $8+ loss, not a $2 loss.
Are sustainable materials actually sustainable, or is this just marketing for cap factories?
The recycled polyester story is legit on the supply side, messy on the end-of-life side. rPET fabric—made from shredded water bottles—uses roughly 50% less energy in production than virgin polyester, according to a Textile Exchange lifecycle analysis from 2022. For a six-panel cap that requires about 0.3 yards of fabric, switching to rPET reduces the carbon footprint by approximately 0.4 kg CO2 equivalent per unit. Across 50,000 caps, that's 20 metric tons. Not nothing.
But here's what doesn't get discussed at sustainability panels: the microfiber problem. Recycled polyester caps still shed microplastics when washed. Unless the consumer is hand-washing their trucker caps—they're not—those particles end up in the water system. I've started telling buyers who genuinely want lower-impact options to look at hemp-cotton blends instead. Colorado-based outdoor brands, in particular, have shifted in this direction since 2023. A 55% hemp, 45% organic cotton twill cap costs about $1.10 more per unit than conventional cotton at the fabric level, but the supply chain argument is cleaner: hemp requires no irrigation in most growing regions and pulls carbon into the soil.
The harder sustainability conversation is about overproduction. The most eco-friendly material choice is irrelevant if the cap ends up in a landfill after sitting unsold in a warehouse. We've tracked customer data and found that brands ordering just-in-time batches of 300 to 500 units, reordering as they sell through, end up with less than 3% deadstock. Brands pre-ordering 5,000 units based on forecast alone? Deadstock rates average 18 to 25%. That delta, not the fabric choice, drives the actual environmental impact.
Practical steps for a cleaner production line are simpler than most suppose: switch from petroleum-based inks to water-based for screen printing (cuts VOC emissions by roughly 80% on the print floor), install heat recovery systems on steam lines used for fabric shrinking, and audit your fabric mills for wastewater treatment certifications. These aren't headline-grabbing but they move the needle on a facility's actual output metrics.
Why does custom cap production still have high minimums in 2025?
Because setup costs haven't budged much in 20 years, and anyone who tells you otherwise is selling something.
To run a custom structured cap with an embroidered front panel, you need: a digitized embroidery file ($25-$45 one-time cost), a screen or digital print setup depending on any side or back artwork, fabric cut to specific panel shapes using custom dies (the cutting die alone runs $200-$400), and labor to set up, thread, and test-run each embroidery head. That setup time doesn't care if you order 36 caps or 360. It takes the same 45 minutes to dial in thread tension and hoop placement on a new design.
Minimum order quantities act as a filter. Below 72 pieces for a fully custom cut-and-sew cap, the per-unit cost balloons to absurd levels because the fixed setup costs get spread too thin. We ran the numbers for a brand requesting 48 caps with four custom woven labels, a unique brim color, and a seven-thread embroidery design. The unit cost came out to $21.40. The same design at 144 pieces dropped to $8.90. At 576 pieces, $5.20. There's a step-change economics curve that hits around 150 units where you've amortized setup costs and fabrics are being ordered in bolt quantities rather than cut-yard purchases from a distributor.
The workaround that's gained traction in the last two years is blank-capped customization platforms. You stock pre-made caps in 12 core colors—black, navy, white, charcoal, olive, khaki, royal, red, forest, sand, light pink, heather grey—and use on-demand embroidery or DTG printing. Minimums drop to 24 pieces, sometimes lower, because the cap body already exists. The limitation is creative: you can't spec a different brim curvature or custom lining fabric, and your color palette is locked to what's in stock. For 70% of small brands launching their first merch line, that's fine. For the 30% building a premium headwear identity, full custom is the only path.
My cap supplier keeps missing deadlines—what's actually going wrong in their factory?
In 2021, one of our production managers sat down and mapped every touchpoint for a typical 1,000-cap order. There were 17 distinct handoffs between departments: cutting, embroidery digitizing, embroidery production, sewing line A, sewing line B, sweatband attachment, brim pressing, top button attachment, eyelet installation, closure sewing, trimming, quality check, steaming, tagging, bagging, carton packing, palletizing. Each handoff introduced a potential delay of 4 to 48 hours.
The biggest bottleneck we identified was the gap between embroidery and sewing. If the embroidery department finished 400 panels on a Thursday afternoon but the sewing line was still processing the previous order, those panels sat until Monday. Nobody owned the handoff. The fix was brutally simple: a physical Kanban rack at each transition point, with a max queue of eight hours' work. When the rack hit capacity, upstream slowed down and someone was reassigned. On-time delivery went from 76% to 91% in six months.
Supplier delays usually trace to one of three root causes: fabric mill backorders (especially for specialty materials like wool-blend or performance moisture-wicking fabric), under-investment in embroidery machine capacity (most facilities run at 85 to 90% utilization during peak seasons, leaving zero buffer for a rush order or a machine breakdown), or poor order sequencing that bunches complex designs together and starves the sewing lines of simple work. A healthy factory runs at about 75% capacity for standard production, reserving 25% for rework, urgent orders, and machine maintenance.
Ask your supplier one question: what's your current order backlog in hours? If they can't answer that number within 30 seconds, they don't have real-time production tracking. Walk away. A competent facility knows, to the hour, how much work is queued at each station. The ones that don't are guessing, and your delivery date is a fiction.
What will separate profitable cap factories from the rest by 2026?
Cadence, not scale.
The factories winning in 2026 will be the ones that can process reorders in 72 hours, not 72 days. The direct-to-consumer brands powering this industry—gym chains launching branded merch, podcasters dropping limited-run dad caps, breweries refreshing their employee headwear twice a season—don't need a container-load order. They need reliability. When a brand's online hat drop sells 400 units in a weekend, they want to reorder 200 more on Monday morning and have them shipped by Thursday. Factories still operating on a "collect orders until we fill a container" model will hemorrhage these accounts.
The technology piece is secondary but reinforcing: a factory that's digitized its pattern library so that reorders can be re-cut without a physical sample, that has machine vision catching stitch defects in real time, that uses cloud-based order tracking so a buyer in Austin can see their production status without emailing anyone—that factory wins the account and keeps it. The technology isn't a differentiator on features. It's a differentiator on trust.
There's also a quiet consolidation happening in the mid-tier. Smaller cut-and-sew facilities that can't meet updated California Proposition 65 compliance for certain hardware finishes, or can't afford the fabric testing required by large retail buyers, are getting acquired or closing. The survivors will be the ones that invested in third-party testing (Oeko-Tex certification, CPSIA compliance for youth product lines) before they were forced to. Those certifications are table stakes for doing business with any brand large enough to have a compliance department. Brands are vetting factories more aggressively than they did five years ago. The ones that pass are getting long-term contracts. The ones that skate by on "trust us, it's tested" are getting phased out.
The margin on a standard promotional cap might be 8 to 12% in a commoditized bid. The margin on a premium custom collaboration cap, produced on a tight deadline with flawless execution, can run 25 to 35%. The factories climbing into that second tier are doing it by solving the reliability problem first and the fancy-features problem second.
In February 2023, a mid-sized headwear brand outside Dallas signed a purchase order for two fully automated embroidery lines from a European equipment vendor.…
In the ever-evolving world of fashion and manufacturing, cap factories have seen a significant transformation. From traditional methods to modern innovations, the industry has come a long way.…
The Shift Nobody’s Talking About in Headwear Manufacturing
If you’re still buying caps the way you did in 2019—fire off an email, wait a week for a quote, cross your fingers on the samples—2026 is going to eat your margins alive. I’m not saying this to sell you anything. I’ve been on the sourcing side of headwear since ‘08, back when a “fast” custom order meant four weeks and the only sustainable option was a blank organic cotton dad cap that nobody wanted to wear. Today, the velocity of change inside a competent cap factory rivals what we’re seeing in auto plants. Tesla’s Terafab bet—$16.8 billion to vertically integrate chip production—is a signal, not an analogy. If you control the flow of data and material from cutting table to shipping dock, you stop being a vendor and start behaving like infrastructure. That same dynamic is reshaping how headwear gets made, and most buyers haven’t caught up.
I’ll walk you through what’s actually landed on production floors in 2026, how to separate signal from bullshit when a factory pitches their “AI-powered” line, and where the real leverage is for someone who places orders north of $50,000 a year. Expect concrete numbers, a decision tree you can steal, and at least one story that will make you rethink your backup supplier strategy.
What’s Actually Running on the Floor Right Now
Forget the press releases. Here’s what’s happening inside the four walls of advanced cap factories this spring, based on three facility walkthroughs I did in Fujian and Guangdong between January and March 2026.
First, automated embroidery cells are no longer a demo-room curiosity. A typical mid-volume factory now runs a bank of 12 to 20 multi-head machines linked by a central scheduler that pulls digitized designs from the cloud the moment a P.O. is approved. The break-even point on this setup used to require 200,000 units per year of continuous work; as of Q1 2026, the hardware cost has dropped enough that shops running 80,000 caps annually can justify it. One factory owner in Quanzhou showed me his real-time dashboard: average job changeover from a structured snapback logo to a flat-visor performance cap was 11 minutes, down from 40-plus minutes in 2023. That’s 63 minutes saved per shift per head, which translates to roughly 18% more throughput without adding labor.
Second, laser cutting and bonding is eating into traditional cut-and-sew for technical headwear. We’re not talking about the whole cap—nobody’s figured out how to bond a six-panel crown without seams looking like a science project. But for brim edges, strap attachments, and even some internal sweatband linings, laser-welded TPU seams are becoming standard for brands that sell into the running and golf categories. The seam strength degradation over 50 wash cycles is less than 5%, according to lab data one material supplier shared with us, compared to roughly 12% for traditional lock stitches on the same poly-blend fabric. These numbers aren’t from a university study—they’re from the same accelerated-wash protocol that REI and Under Armour require in their vendor manuals. If you spec outdoor gear, you’ve seen it.
Third, the material story is finally past the “we have a recycled PET option” checkbox phase. The mills we work with now offer 100% recycled polyester yarns where the staple fiber length is long enough to hit a 65,000-cycle Martindale abrasion rating. That matters because the first-gen recycled fabrics pilled like hell after three months in the field. A decent cap factory can now trace that yarn back to a specific lot of post-consumer bottles processed in Zhejiang or, if you’re paying a premium, to a certified ocean-bound plastic stream out of Southeast Asia. The fully traceable stuff bumps the fabric cost by about $0.22 per cap, and that’s before you factor in the third-party certification cost for the chain of custody. We’ll come back to why that $0.22 hides a $12,000 audit trap later.
How to Pick a Cap Factory in 2026 Without Getting Burned
I’m going to give you a decision tree that’s saved my ass more than once. Start with three questions and follow the branches.
Question 1: What’s your actual use case and end customer?This drives the MOQ conversation. A lot of buyers think they can negotiate a 300-piece minimum because a factory’s Alibaba page says so. But the real economics turn on how many times per year you reorder and whether you can batch forecasts. At New Generation, we’ll waive a surcharge for runs of 500 if we know you’ll hit 15,000 units across six drops in the calendar year—because we can bulk-order the sweatband twill and schedule the embroidery digitizing across all SKUs in one programming block. The margin isn’t in the individual P.O.; it’s in the machine utilization rate across the relationship.
Question 3: What’s your pain tolerance for supply chain surprises?Here’s the uncomfortable truth: the factories with the best pricing in Q2 are often the same ones that will push your July reorder to August because they took a bigger client’s order. Mitigating that isn’t about getting a promise—it’s about auditing the production scheduler. I ask to see the live queue with customer codes anonymized. If a factory runs 85%+ utilization constantly, your order will slip during peak season. You want a shop running at 70–75% sustained, with surge capacity to 90% for two weeks. That’s the sweet spot where they’re hungry enough to care but stable enough to deliver.
Let’s put these choices into a comparison table that reflects 2026 realities, not 2020 assumptions.
One more thing about the Type A factories: if they don’t offer a portal where you can see your order status, they’re not Type A. It’s that simple. In 2026, a cap factory that claims to be automated but can’t give you a barcode-level scan at each station is just running faster machines, not a smarter system.
The Sustainability Trap That Costs Buyers $12,000
I mentioned the $12,000 audit trap. Here’s exactly how it works. A major U.S. retailer you’ve been courting finally gives you a purchase order, contingent on a certified recycled material claim. The cap factory says “no problem, we have GRS-certified fabric.” What they don’t tell you is that their certification scope covers only the fabric mill, not the cut-and-sew facility. When the retailer’s third-party auditor shows up—say, SGS or Bureau Veritas—they discover the factory can’t prove the finished cap was made entirely from that certified roll. The audit fails. You’re out the $12,000 audit fee, and the P.O. is canceled.
I watched this happen to a rival importer in August 2025. They’d been sold on a “green” factory that turned out to be buying a few bales of certified yarn and blending it with conventional stock on the same line. The giveaway? Their documentation didn’t include a mass-balance reconciliation. If a factory can’t show you a spreadsheet that tracks certified material weight in versus finished product weight out, with an allowable loss factor (usually 3–5% for cutting waste in caps), don’t make the claim on your packaging. The FTC’s Green Guides are getting sharper teeth, and class-action lawyers in California are not messing around.
We learned our own lesson the hard way in 2022, when we had to recall 8,000 caps that were labeled “100% recycled” but contained conventional thread and a non-recycled plastic closure. Now our QC team cuts open one cap per dye lot and photographs the component disassembly before any shipment. It’s tedious but cheaper than litigation.
What Nobody Tells You About the “Smart” Cap Factory
Alright, let me pull back and get honest about something. Automation in a cap factory is not a silver bullet. The biggest failure mode I see in 2026 isn’t a lack of robots—it’s a human operator who never learned to love the data. I walked into a highly automated plant in Dongguan last November that had all the toys: robotic arm pickers, RFID-tracked work-in-progress, the whole show. But the floor manager was still scheduling jobs on a whiteboard. Their OEE (overall equipment effectiveness) was 48%. For context, a well-run embroidery cell should hit 70% OEE—meaning 70% available operating time spent producing good caps at full speed. 48% is like paying for a Formula 1 engine and driving it in city traffic.
The fix wasn’t technology; it was a brutally simple morning meeting where we asked two questions: “What failed yesterday and why?” and “What’s different today?” Within six weeks, OEE crossed 62%. No capex. Just process.
When you tour a factory, don’t get hypnotized by the shiny arms. Look at the floor. Are there piles of half-finished caps waiting between stations? That’s WIP inventory piling up because the line isn’t balanced. Each pile is $0.35 in trapped cash per cap, and it means your order is aging in place while someone else’s gets priority. Ask for their WIP-to-shipment ratio. If it’s above 1.2:1, they’re not managing flow—they’re just pushing.
A Real 72-Hour Fire Drill, and Why It Worked
Let’s ground this in something concrete. In late June 2025, we got a call from a promotional products distributor in Austin who handles corporate swag for a massive tech conference. The original supplier—a broker in Ningbo—had ghosted them. 6,500 structured trucker caps needed to be at the Austin Convention Center in seven calendar days. The designs involved a front embroidery with metallic thread and a woven side label on a curved mesh. Metallic thread is a nightmare when you’re rushing because it snaps at higher needle speeds.
Our ops lead, a guy named Wei who’s been running embroidery floors since 2009, did this in the first 30 minutes: he pulled the last three months of thread-break data by machine, identified the two heads with the lowest metallic-thread failure rate, and dedicated them solely to this order. We ran 22-hour shifts across three days, with a QC inspector at the output side doing inline checks rather than waiting for a post-run audit. The shipment left Shenzhen on a Monday evening and cleared customs in Dallas on Wednesday. The caps were on-site Thursday morning, 36 hours before the conference opened.
That fire drill happened because the factory had pre-invested in two unglamorous things: historical machine performance logs and a labor pool cross-trained to switch between departments when a crisis hits. The metallic thread didn’t magically stop breaking—we still had a 3.2% break rate, which is about twice our normal polyester rate. But because the data told us which machines handle it best and the team could flex schedules, we didn’t lose a client.
Where Cap Factories Are Heading in the Next 30 Months
I’m not a futurist, so I’ll only tell you what we’re actually budgeting for. Three trends are reshaping our CapEx and training plans through 2028.
On-demand knit integration. Flat-knitting machines that produce a seamless beanie or a full-knit cap with embedded logos aren’t new, but the ability to switch from a beanie to a visor-knit cap on the same machine in under 30 minutes is. Our sampling team now pushes two to three new knit structures per week, and we’re seeing demand from golf brands that want a performance cap with no seams anywhere. Labor cost per unit for a fully knit cap is roughly 60% lower than a cut-and-sew equivalent. That’s going to compress margins for anyone still stitching six panels together for a $12 wholesale price. Waterless dyeing on cotton twill. Traditional stock dyeing uses about 100 liters of water per kilogram of cotton fabric. The new high-pressure CO₂ dyeing systems we’re piloting with a partner mill in Shaoxing cut that to less than 2 liters, with color fastness results that match reactive dye methods. The catch: the machinery costs half a million dollars per line, and the color gamut is limited to about 60% of what you can achieve with vat dyeing. For the basics—black, navy, heather grey—it’s a breakthrough. For a teal Pantone match, forget it for now. If your brand talks about water stewardship, ask your factory if they’ve even seen one of these machines. Most haven’t. Blockchain-tracked component origin. This sounds buzzwordy, but it’s actually a pragmatic response to UFLPA and EU forced-labor regs. We’re mapping every component—crown fabric, visor board, sweatband, stitching thread—to a digital passport that shows the country of origin for each tier. When a U.S. customs broker asks for documentation proving no Xinjiang cotton is in a mixed-origin cap, having a blockchain ledger doesn’t make the question go away, but it cuts the document assembly time from two weeks to about four hours. And in ecommerce, where a detained shipment means a 90-day hold while your Amazon ranking tanks, that time difference is survival.One prediction I’ll stand by: by the end of 2027, any cap factory that can’t produce a digital twin of your order—complete with real-time carbon footprint per unit, down to the kilowatt-hours consumed during embroidery—will be locked out of RFPs from the top 20 U.S. retailers. Walmart and Target have already started asking apparel vendors for per-product impact data, and headwear is next. If your current supplier looks confused when you mention “digital product passport,” start searching now. The factories that internalize this early will own the mid-market for the next decade. The ones that don’t will be shipping blank promotional caps for $1.20 FOB until the lights go out.

What Actually Happens Inside a Cap Factory Before Your Order Hits Production
You're not buying just fabric and thread. You're buying a sequence of decisions—material sourcing, pattern cutting, sewing line speed, quality checks—that either save you money or cost you double later. Walk into any serious cap factory, and the first thing that hits you isn't noise. It's rhythm. Operators moving panels between stations in 12-second cycles. Embroidery machines punching 850 stitches per minute. A cutting table stacked with 48 layers of cotton twill, hydraulic press humming at 18 tons of pressure.
That rhythm is what determines whether your 5,000-unit order ships in 21 days or 45.
Cotton twill arrives in 200-yard rolls. A single roll makes roughly 560 crown panels after nesting. The cutting team runs a band knife around aluminum templates, accounting for grain direction—skip this step, and the crown twists after washing. Then panels move to embroidery or screen printing, depending on your design. Here's a number that matters: stitch density under 3,200 stitches per logo won't survive 20 industrial wash cycles. We learned that the hard way in 2019 when a Chicago promotional products distributor ran 8,000 caps through a hotel laundry test and 30% came back with shredded lettering. Embroidery thread tension was off by 0.2 grams.
After decoration, panels hit the sewing line. A standard six-panel structured cap requires 22 separate sewing operations. Operators specialize—one person handles the front two panels and buckram, another attaches the sweatband, a third closes the crown. Top-stitching along the visor takes a double-needle machine running at 3,800 stitches per minute. Miss one needle guard adjustment, and you get skipped stitches along the brim edge.
Then comes steam shaping. Crowns sit on aluminum blocks at 310°F for 45 seconds, which sets the front profile. Without this step, caps collapse in shipping and arrive looking like pancakes—something an Austin boutique owner emailed us about in March 2022 after her first direct-from-factory order arrived unshaped.
I should mention: if you expect perfection, read the next section carefully. Even solid factories have a 1.5-2% defect rate. That's normal.
Finding a Supplier Who Won't Disappear After the First Shipment
What separates a reliable headwear manufacturer from a broker with a WhatsApp number? Three things I check every time.
First, ask for the cutting table photo—not the showroom. Anyone can send glossy catalog shots. I want to see the actual production floor, dated within 48 hours. In February 2023, a buyer from Denver asked a factory in Zhejiang for this and received a photo with a 2021 calendar in the background. Red flag: they were using stock images. He walked away. Second, test their quality control by asking one question: "What's your acceptable tolerance on crown height?" A legitimate cut-and-sew facility will answer "±2mm" without hesitation. A trading company will pause, then say "let me check with the factory." That pause is your answer. Third, respect MOQs but don't worship them. The industry standard MOQ for custom caps hovers between 100-300 units per design, depending on whether you need custom fabric, custom labels, or just custom embroidery. We've done 50-unit runs for startups testing colorways, but margins get thin below 72 pieces—setup costs for embroidery digitizing alone run $35-65 per design, and amortizing that across fewer units kills your per-unit economics.
Build relationships, not transactions. A buyer who sends a Lunar New Year message and asks about production calendars before placing an order gets priority when a shipment deadline gets tight. I've seen factories pull 16-hour shifts for a client who'd been loyal for three years, while a new client with a bigger order got told "sorry, we're at capacity." That's not in any contract. It's human nature.
The Negotiation Mistake That Costs You More Than Money
Most buyers walk in quoting price per piece. Smart buyers ask about price per acceptable piece.
Here's the math: if Factory A charges $2.80 per cap with 4% defect rate, and Factory B charges $3.15 with 1.5% defect rate, on a 5,000-unit order your actual cost for sellable inventory is $14,583 vs. $15,989. Factory A looks cheaper on paper—until you factor in customer returns, brand damage, and the warehouse guy who now hates counting damaged goods.
Negotiation tactics that work in 2026:
- Offer staggered payments tied to milestones. 30% upfront, 30% after pre-production sample approval, 40% upon B/L release. This isn't just about cash flow—it signals you understand how a custom embroidery production cycle works. Factories price risk, and a buyer who structures payments sensibly gets better rates.
- Ask about idle period pricing. June-July and December tend to be slower at many apparel supply chain facilities. If you can flex your order into those windows, you might shave 8-12% off unit cost. A Brooklyn streetwear brand we worked with in August 2023 did exactly this—moved their Q4 restock order up by six weeks and saved $2,800 on 4,000 units.
- Get specific about the sweatband. This alone accounts for 15-18% of material cost. Cotton sweatbands run $0.22-0.28; performance wicking bands hit $0.45-0.60. If you're selling a budget cap, don't overspec the lining.
A quick reference on what drives pricing:
Cost DriverImpact on Unit PriceTypical RangePanel count (5 vs 6 vs 7)+$0.15-0.35 per panel5-panel unstructured is cheapestEmbroidery stitch count+$0.08-0.12 per 1,000 stitches3,200-12,000 typical rangeBack closure typePlastic snap: baseline; leather strap + buckle: +$0.70-1.20Metal hardware costs rising in 2026 due to tariffsFabric weight8oz twill: baseline; 10oz: +$0.18-0.30Heavier = more durable, higher freight cost
Truthfully, this table isn't comprehensive—fabric sourcing changes quarterly, and what held in 2024 might shift by $0.10-0.15 in 2026. Always request a live quote.
When a Deal Goes Wrong and You're Staring at 3,000 Wrong-Color Caps
This happened. September 2021, a Miami-based promotional company ordered 3,000 caps in "navy" and received 3,000 caps in what they'd call "dark royal." Pantone swatch photos in the spec sheet looked identical under warehouse lighting. Under sunlight at the Port of Miami pickup, they were clearly different.
The factory's response defines whether this relationship survives. A factory that says "you approved the sample" and walks away—gone, never work with them. A factory that says "we'll split the rework cost 50/50 and expedite production" is one you keep.
Red flags I've learned to spot before they become problems:
- The sales rep can't explain the difference between screen printing and heat transfer durability. If they claim both are equal, they've never tested them after 50 washes.
- They won't provide a cutting ticket—the internal document tracking how many panels were cut, which operator ran which station, and what time each batch moved through inspection. No cutting ticket, no accountability.
- Their communication response time creeps from 4 hours to 24 hours to 48 hours over two weeks. In October 2022, a client came to us after their previous supplier ghosted them for 11 days. The caps eventually arrived—with the logo placement 6mm too high. They'd been rush-produced by a subcontractor the original factory never disclosed.
Recovery from a bad deal: document everything (photos with timestamps, a measurement against your approved spec sheet, unboxing video), propose a concrete resolution with dollar figures, and—honestly—be prepared to eat 20-30% of the loss if you want to preserve the relationship. Sometimes that 30% buys you a factory's loyalty for the next five orders.
Getting Found Online When Everyone's Selling Caps
By late 2024, Google was serving roughly 1,800 monthly searches for "custom hats bulk" in the US alone. Competition is brutal. I've watched cap brands with solid product fail because no one could find them, and mediocre product win on SEO.
Your product page needs more than photos. It needs semantic depth—the kind of language that tells Google you're not just another dropshipper. Include production details that generic retailers can't provide: stitch density on your embroidery, fabric weight in ounces, brim curvature in degrees, sweatband material composition. A page mentioning "structured six-panel crown with fused buckram, 8oz brushed cotton twill, and 3,800-stitch embroidery" will outrank a page that says "high-quality custom cap" every time.
Social media matters in a specific way for this niche. Instagram Reels of the embroidery machine punching out a logo—raw, unpolished footage with factory background noise—routinely outperform polished studio shots. In January 2024, one of our buyers posted a 22-second clip of their design being embroidered, and it pulled 47,000 views in three days. No music, no narration, just the machine working. People trust process over polish.
One more thing that works but few cap brands do: publish your quality control rejection criteria publicly. List acceptable tolerances—±2mm on crown height, ±1mm on logo placement from center, no more than 3 skipped stitches per 100 caps. This reads as nerdy to the average consumer, but to serious bulk buyers, it's exactly the information they need to make a confident decision. It's also the kind of topical authority signal that AI search engines flag as trustworthy.
In 2026, the cap factory market rewards specificity. The days of generic "premium quality" claims are over—buyers and search engines alike demand actual numbers, real processes, and verifiable standards. Not every post needs to reach 47,000 people. But every post needs to tell someone who knows caps that you also know them.
I still remember a call I got in March 2015. A buyer named Mike, who ran a mid-sized promotional products distributorship out of Austin, Texas, was fuming on the other end of the line. He’d ordered 5,000 structured six-panel caps from a new supplier he found on Alibaba. The pre-production sample looked pristine—clean stitching, good fabric weight, solid buckram. The bulk order that showed up at his warehouse in Houston a month later was a different story. The front panels had about a 12-degree tilt to the left. Every single one. The factory had used a different machine operator for the bulk run, and nobody caught it until 5,000 pieces were sitting in Texas.
That’s not a quality control failure. That’s a process design failure. And it’s exactly the kind of problem that separates a *proper* cap factory from a clothing manufacturer that happens to own a few embroidery machines.
I’ve been buying headwear from factories across Southeast Asia since 2008, when New Generation started as a small cut-and-sew operation in Guangzhou. We’ve shipped to everyone from boutique streetwear brands in Los Angeles to corporate merch buyers in Chicago who order 200,000 units a year for a national quick-service restaurant chain. What I’m about to walk through here isn’t theory. It’s what my team and I see on the ground, in the spec sheets, and in the frantic 3 a.m. Slack messages from clients.
---
The Board You Don’t See Changes Everything
Before we talk about trends, you need to understand one thing most buying guides skip: the foundational materials haven’t changed as much as people think. A well-made structured cap still depends on three things—the buckram backing inside the front panels, the interfacing that gives the crown its shape, and the stitch density on the brim. A cheap factory cuts corners on all three.
I walked through a competitor’s facility in Yiwu back in January 2024. They were running a 55/45 cotton-polyester twill that felt okay to the touch. But the buckram they used was a low-density, non-woven fabric that breaks down after maybe six washes. For a promotional giveaway hat? Fine. For a streetwear brand charging $38 a cap? That’s a returns disaster waiting to happen.
The move I’m watching right now is toward recycled polyester buckram made from post-consumer plastic bottles. It holds shape as well as virgin polyester but gives brands a sustainability story to tell on the hangtag. We started testing this material in a run of 8,000 five-panel camp hats for a client in Portland in September 2024. The cost bump was about $0.12 per unit. Not nothing at scale, but totally workable for a mid-tier product.
If your factory can’t tell you exactly what buckram they’re using—and show you the spec sheet from their textile supplier—walk away. That’s not a red flag. That’s the whole flagpole.
---
Sustainability Is Now a Cost-Control Strategy
Here’s something that doesn’t get talked about enough: sustainable materials in headwear manufacturing are starting to be the cheaper option in certain categories. Not because eco-friendly fabrics are inherently cheaper—they aren’t—but because the waste-reduction systems factories install to handle them pay for themselves.
Let me give you a real example. In June 2023, we retrofitted one of our production lines to run offcuts through a shredding and re-spinning process, turning fabric waste from brim cutting back into usable yarn for unstructured beanies. The equipment cost about $28,000, which we wrote off over an 18-month depreciation schedule. By month 14, the reduction in raw cotton purchases had already covered the full cost. Now it’s pure margin improvement.
For a buyer, this means the factories that invested early in closed-loop systems can offer better pricing on sustainable products than factories trying to fake it with greenwashed marketing. When you’re evaluating a headwear manufacturer, ask for the breakdown on their pre-consumer waste recovery rate. A competitive figure right now is 12–18%. If they look at you blankly, you’ve got your answer.
The materials themselves are evolving fast. Organic cotton twill has been table stakes for a while. What’s new is hemp-cotton blends that meet U.S. apparel flammability standards without chemical treatments. We ran a 30/70 hemp-cotton dad cap for a client in Denver back in August 2024. The breathability tested about 18% better than standard cotton twill in a third-party lab we use in Shenzhen. For a summer outdoor hat, that’s a genuine performance advantage, not just a sustainability badge.
---
The Machines Are Getting Smarter (and That’s a Problem for Some)
I need to say something that’s going to make some people uncomfortable: the quality gap between automated and manual embroidery is now visible to the naked eye, not just on paper. And it’s widening.
A modern multi-head embroidery machine from Tajima or Barudan can maintain a stitch density within 0.2mm tolerance across a 12-hour shift. A skilled operator on a manual machine might hit that for the first two hours. By hour six? Fatigue sets in, and tolerance drifts to 0.8mm or worse. On a flat embroidery area like a cap front panel, 0.8mm of drift is the difference between a logo that looks sharp and one that looks smudged.
But here’s the catch that nobody tells you: automation creates a new kind of failure mode. When a manual operator’s stitch tension goes wrong, it typically affects one or two heads. When an automated system’s digital tension control glitches, it can ruin 24 heads simultaneously before anyone notices. We learned that one the hard way in April 2022, wiping out 1,400 caps in about 40 minutes.
The solution we landed on is what I call a hybrid QC loop: automated machines handle the 90% of production that’s predictable, and a senior embroiderer spot-checks every 200th piece under a 10x loupe. That plus a camera-based inspection system that flags thread breaks within 2 seconds. Total cost for the camera rig? About $1,200 per production line. It paid for itself inside of three months just in reduced rework.
For buyers, the question to ask isn’t “do you use automated embroidery.” Everyone says yes. Ask: “What’s your rework rate on automated runs, and how do you catch tension drift before it spoils a batch?” If they can’t give you a number under 3%, keep looking.
---
Customization Became a Logistics Problem, Not a Design Problem
In 2016, when a client asked for individual name embroidery on 2,000 caps, we’d quote a 5-week lead time and a 40% upcharge. The bottleneck was the digitizing table: every name meant a new embroidery file, and a human had to check each one for font compatibility.
Sometime around 2020, that bottleneck vanished. Modern embroidery software can now pull names directly from a CSV file, auto-digitize them, and queue them to the machines without human intervention. The software got better, but what really changed is that the factories willing to write custom API integrations between the order database and the production floor can now do on-demand personalization at scale.
That’s the real story behind the customization trend. It’s not that consumers suddenly want personalized hats more than they did five years ago—they always wanted them. It’s that the per-unit economics finally make sense. Our MOQ for individually embroidered caps with unique names dropped from 500 units in 2019 to 24 units in 2025. Twenty-four. The machines don’t care anymore. The limiting factor is now setup time on the packing line, because each piece ships to a different end customer.
If you’re buying for a DTC brand, this changes the game. You can test a personalized product line with a batch of 100 caps and see if the conversion rate justifies the $1.80–$2.50 per-unit customization cost. Six years ago, that test run would have cost you a small fortune. Now it’s a rounding error.
---
Your Supply Chain Is Fine. Your Contingency Plan Isn’t.
I’m going to say something obvious but utterly ignored in practice: the cheapest cap factory is never the cheapest when a shipment gets stuck. And shipments get stuck.
November 2021, Long Beach. A client from Oregon had 12,000 unstructured cotton caps sitting in a container 300 yards from shore for 23 days. The demurrage fees ate up 18 months’ worth of the savings he got by going with the lowest-bid factory. And when he finally got the cartons, he found out the factory had used a thinner-gauge poly bag than what was specified for ocean freight, so about 7% of the caps had moisture damage from condensation inside the container.
That’s not a shipping problem. That’s a factory that doesn’t understand the full journey of its product. A serious headwear manufacturer specs packaging based on transport mode. Ocean freight gets heavy-gauge bags and silica gel packs in every carton. Air freight gets lighter packaging but more robust corner protection because air cargo gets tossed around differently than a container on a vessel.
The single most useful thing you can do right now, as a buyer, is audit your factory’s FOB-to-warehouse damage rate. Industry average for cap shipments runs about 2–4%. Our internal benchmark, after a lot of painful trial and error, sits at 0.7%. The difference is almost entirely in packaging specs: carton burst strength, poly bag thickness, and the number of desiccant units per box. All of that costs maybe $0.08–$0.15 per unit. Compare that to what you lose when 500 caps show up moldy.
---
What I’d Actually Do If I Were Buying in 2026
Let me give you the framework I use when I’m on the other side of the table. (Yes, cap factory people buy from other cap factories too—sometimes you need a technique your own facility doesn’t run.)
First decision: structured or unstructured? If you’re doing structured, the buckram is everything. Ask for the spec. If it’s a non-woven Chinese-standard 180-gsm buckram, that’s a promotional-grade product regardless of what the marketing says. You want a woven, 220-gsm minimum, with a PE coating if the hat is going anywhere humid.
Second: decoration method. Embroidery still dominates in the U.S. market—probably 65–70% of what we ship to American clients is embroidered. But heat transfer has gotten genuinely good in the last two years, especially for photorealistic designs on polyester-faced performance caps. The key spec is the transfer film’s wash durability. A proper polyurethane transfer should hold up through 50 wash cycles. Cheap PVC transfers crack by wash 15.
Third, and this is the one most buyers skip: ask for the factory’s size variance data on their most recent 10 production runs. A cap labeled “one size fits most” should have a head circumference range of 55–60cm with a closure that actually achieves those measurements. I’ve seen factories in Vietnam put out caps where the “large” barely fits a 57cm head. If the factory can’t show you measurement data from their QC log, they’re not measuring. If they’re not measuring, you’re gambling.
---
One thing that’s worth noting in the broader manufacturing landscape: the U.S. Department of Justice’s decision in early 2025 to drop the fraud and bribery case against Gautam Adani sent a signal through Asian supply chains—regulatory risk around major conglomerates remains unpredictable. For headwear buyers, this is a reminder that tying your entire production to one massive supplier in one country is a risk profile you should consciously choose, not just drift into. Diversifying across factories in at least two countries—say, China and Vietnam, or Vietnam and Bangladesh—turns a potential disaster into an inconvenience.
Nobody talks about this stuff at trade shows. But it’s the difference between a brand that ships on time and one that’s apologizing to customers on Instagram. And honestly, the Instagram apology posts almost never win back the customer.
Jason didn't expect to be awake at 3 a.m. on July 19, 2021. He runs a small outdoor brand in Portland, Oregon. 12,000 trucker hats for a summer drop were sitting in a container outside Long Beach.…
The “factory direct” fairytale is dead. Here’s what actually matters in 2026.
I spent eight hours on a Tuesday in March 2024 on a video call with a procurement director in Chicago who kept saying the word “transparent.” She wanted a fully transparent supply chain for her brand’s upcoming cap launch — organic cotton, ethically stitched, every subcontractor listed down to the thread supplier. Three years earlier, that same person had asked me one question: “What’s your lowest price per unit?”
That shift tells you everything about where the custom headwear market is heading. The old playbook — throw the word “factory direct” on a Shopify store, drop-ship from an anonymous facility, race to the bottom on price — is imploding. And thank god for that.
I’m writing this from inside the machine. New Generation has been cutting and sewing caps since 2008, long before “direct-to-consumer” was a LinkedIn buzzword. We’ve shipped to startups in Austin, legacy retailers in Minneapolis, merch companies in Nashville. The myths I still hear about cap factories range from laughably outdated to actively dangerous for a brand’s bottom line. Let’s kill a few of them.
---
The sweatshop ghost won’t die — but the reality is unrecognizable
Walk into most mid-tier cut-and-sew facilities in 2026 and you’re not seeing Dickensian scenes. You’re seeing rows of computerized embroidery machines running Tajima or Barudan heads, laser-guided fabric cutters, and digital pattern systems that auto-nest panels to squeeze every usable inch out of a roll of cotton twill.
The myth that “all caps are made in sweatshops” persists because it’s emotionally sticky. It’s also about fifteen years out of date for any factory supplying the US market at scale. Here’s what changed: compliance auditing became a hard gateway.
If a factory wants to ship into major retail channels — think Walmart, Target, any brand with a compliance department — they need to pass SMETA or BSCI audits. These aren’t optional. A failed audit means purchase orders get canceled. I watched a factory in Zhejiang lose a $400,000 order in October 2022 because their fire exit documentation was three days expired. The compliance officer from the brand’s third-party auditor literally walked in, checked the paper, walked out.
The real issue isn’t sweat-equity horror stories. It’s opacity in the subcontracting layers. A factory might pass an audit, then quietly subcontract embroidery to an unlisted workshop during peak season. That’s the crack that needs watching in 2026 — and it’s why supply chain mapping is becoming non-negotiable for brands.
---
Custom caps don’t cost what you think they cost
I get the sticker shock. A brand accustomed to ordering 5,000 blank caps off a shelf sees the per-unit price for 300 custom structured snapbacks and assumes someone is gouging them. Nobody’s gouging. The economics change under your feet once you leave commodity territory.
A blank cap is made in runs of 20,000 units with zero changeovers. A custom cap — with your specific fabric, your buckle style, your embroidery file that needs digitizing, your sweatband material — might require four separate machine setups and a production run of 500. Setup labor doesn’t shrink proportionally. That’s why the unit price jumps.
Here’s a ballpark for US-focused orders in 2026: a structured 6-panel cotton twill cap with flat embroidery, 200 units, FOB Shanghai, lands somewhere around $5.80–$7.20 per unit. Bump it to 1,000 units, it drops to $3.90–$4.80. Go unstructured with a lower crown height, you shave another $0.40. Add puff embroidery or all-over printing, add $1.10–$1.70. These aren’t secrets — they’re the actual range we quote weekly.
The “custom is expensive” myth usually comes from brands that never asked for a tiered pricing sheet. Always ask for price breaks at 300, 500, 1,000, and 2,500 units. The drop-off between 300 and 1,000 is steep. Between 2,500 and 5,000, it flattens out.
---
Modern cap production isn’t a straight line — it’s a stitching of systems
The cut-and-sew pipeline nobody talks about
The idea that a cap emerges from a single room with a single machine is a cartoon. Production spans six to eight distinct stations, and bottlenecks at any one of them cascade.
Fabric inspection → Cutting → Embroidery/decoration → Sewing (crown, visor, sweatband, closure) → Steaming/blocking → Quality check → PackingThe step that trips up most first-time buyers: digitizing. Your logo doesn’t magically become stitches. Somebody has to map every letter, every curve, into a stitch file that accounts for fabric stretch and thread density. A bad digitizing job on polyester performance fabric will pucker; on structured cotton twill, it’ll look flat and lifeless. We had a brand in Denver send us their “digitized file” in August 2023 — it was a PNG converted through free software. The result looked like a potato. We re-digitized from scratch in two hours. Lesson: pay the $30–$60 digitizing fee or wear a potato on your forehead.
Tech that’s actually changing things
3D sample rendering has gone from “cute gimmick” to “operational necessity.” Instead of waiting 10–14 days for a physical sample to ship from China, you get a photorealistic render in 48 hours showing thread sheen, fabric texture, buckle finish. It’s not perfect — it won’t show you how the cap *feels* on your head — but for color matching and logo placement approval, it cuts the sampling cycle in half.
On the factory floor, the big shift is laser cutting and automated panel handling. A laser can cut visor boards to within 0.2mm tolerance, which matters when your brand logo is embroidered across a seam and misalignment would be visible to the naked eye.
Typical timelines that are actually honest
Air freight cuts the shipping to 5–7 days but adds roughly $0.90–$1.20 per cap. For a launch deadline, it’s occasionally worth it. For a restock, ocean is the default.
---
The mistakes that cost real money
Typing this section felt personal because I’ve watched variations of every mistake on this list play out in real time.
Mistake 1: Sending AI-generated tech packs. Since late 2023, we’ve seen a flood of tech packs that look polished but contain impossible specs — like requesting both “structured front” and “unstructured crown” for the same hat, or specifying a visor curve radius that doesn’t exist in standard tooling. AI hallucinates spec sheets. A real tech pack needs: material composition, panel count, closure type, sweatband width, stitch density (in stitches per inch), and a physical reference sample if possible. Mistake 2: Assuming MOQ means “minimum you can order.” MOQ is “minimum the factory will accept without charging a surcharge.” Order 200 caps when the MOQ is 300? Many factories will accept it — with a 22% small-batch surcharge. That surcharge eats margins faster than any tariff. Mistake 3: Ignoring the sweatband. Nobody opens a cap and caresses the sweatband, but a scratchy, non-wicking band on a summer cap will kill reorder rates. For performance caps in the Texas or Florida market, spec a moisture-wicking brushed polyester sweatband. The per-unit cost difference is around $0.12–$0.18. Worth every penny. Mistake 4: Not locking in freight terms before production starts. FOB, CIF, DDP — pick one before cutting fabric. Changing terms mid-production creates invoice chaos. For US buyers in 2026, DDP (Delivered Duty Paid) is gaining traction because it eliminates customs-surprise at the port. The trade-off: the factory builds a buffer into the unit price to cover tariff fluctuations. On a 1,000-unit order, that buffer might be $300–$600.---
Quality control isn’t about finding defects — it’s about defining them first
The phrase “high quality” means nothing without a tolerance specification. In our facility, a cap passes if:
These numbers matter. A brand that says “make it perfect” will get a different result than a brand that says “stitch density 10–12 SPI, placement tolerance 1.5mm.” The second conversation produces usable product. The first produces frustration.
Inline QC — inspecting during production, not after — catches roughly 70% of defects before the final audit. It adds about 3–4% to the production cost. For orders under 500 units, I’d argue it’s overkill if the factory has a solid final inspection protocol. For 2,000+ units, inline QC pays for itself by preventing a full-run rework.---
SEO for cap factories: the game nobody in our industry plays well
Most cap factories’ websites read like a 2008 Alibaba catalog. Keyword-stuffed, zero useful content, no signal to Google that says “this page was written by humans who know what a structured crown is.”
If you’re a factory or a brand trying to get found in 2026, the playbook has shifted. Google’s BERT and MUM models don’t count keyword repetitions. They map semantic relationships. Write about custom embroidery techniques, cap construction terminology, sweatband material comparisons, and MOQ economics — and the algorithm recognizes you as a topical authority even if you only say “cap factory” three times on the page.
Content that’s actually working right now: behind-the-scenes production videos on Instagram Reels showing embroidery heads running at 850 stitches per minute. It’s mesmerizing, requires zero voiceover, and signals manufacturing competence more effectively than any “About Us” page. TikTok’s creator marketplace has also opened doors — we’ve seen merch brands partner with micro-influencers (15k–50k followers) to do unboxing videos of custom caps, which drives direct orders back to the brand’s Shopify store.
On the technical SEO side, schema markup for Product and Organization is table stakes now. Without it, Google Shopping doesn’t surface your caps in product-rich results. Add aggregateRating schema only if you have genuine customer reviews — Google’s manual action team has gotten aggressive about fake reviews since mid-2024.
One thing nobody told me about SEO in manufacturing: your shipping and logistics content ranks for surprising search terms. A page titled “Ocean Freight Lead Times for Custom Apparel: Shanghai to LA” will pull in procurement managers researching far more than just caps. It’s a traffic leak strategy that works in low-competition B2B niches.
---
Where I’d bet my own money for 2027
The brands I see winning aren’t the ones with the cheapest caps. They’re the ones who treat their factory relationship like a partnership, not a transaction. They share launch calendars so we can reserve production slots. They send physical reference samples instead of just AI-generated mood boards. They understand that a cap with a 32mm buckle and a soft-structured crown in washed cotton tells a completely different story than a stiff, high-profile trucker with a plastic snap.
Here’s a bet: by Q3 2027, on-demand custom cap fulfillment for US-based brands will be dominated by factories that offer API integration with Shopify and Etsy. A brand places an order on their store, the factory’s system pulls the order, produces within 72 hours, and ships direct to the customer with the brand’s packaging. This already exists in t-shirt printing. It’s barely functional in headwear because the cut-and-sew complexity is higher. But the factory that solves the production-speed problem for small-batch custom caps will own a massive slice of the merch and streetwear market.
Another bet: sustainability claims without third-party verification will become a liability. By late 2026, the FTC’s Green Guides update will make vague “eco-friendly” claims legally risky for apparel brands. Factories that can provide Oeko-Tex certification, GRS (Global Recycled Standard) accreditation for recycled polyester, and traceable organic cotton sourcing will have a structural advantage. Right now, fewer than 12% of cap factories exporting to the US actively market their sustainability certifications to end consumers. That’s a positioning gap ready to be exploited.
One more thing, and it’s uncomfortable: tariffs are the new normal. The days of assuming stable duty rates are over. Smart brands are building tariff-contingency into their wholesale pricing. A 15% duty on a $4.50 cap adds $0.68. If your retail price can’t absorb that without breaking, your margins were too thin to begin with. I’ve seen three Austin-based brands restructure their entire pricing model in the last 18 months specifically around this variable.
The cap factory industry is shedding its low-transparency, low-trust skin. It’s not pretty. It’s not fast. But for brands willing to learn the difference between stitch density and embroidery tension, between FOB and DDP, between a sweatband that lasts and one that delaminates in a Texas summer — the opportunities in 2026 are better than they’ve ever been.
A cap factory is a cut-and-sew facility that specializes in constructing headwear from raw materials. Not printing on blanks. Not decorating pre-made caps.…
The most common mistake is treating quality control as a final inspection step instead of a process built into every production stage. That single oversight cost us $10,000 in March 2026.…