
Visitors walk our floor in Guangdong expecting rows of sewing machines. They get rows of sewing machines.…
The part that decides whether your order ships clean sits 30 centimeters above the needle: a hoop, a piece of 8-ounce cotton twill, and a tension reading that determines whether your front panel is flat in October or puckered by December.
What a Cap Factory Really Sells You Is Tension Control
> A cap factory is a tension-management system. It holds woven or knitted fabric at a controlled stretch, drives thread through that fabric at 750 to 900 stitches per minute, and cools a polyethylene visor into a curve it will hold through two years of daily wear. Everything else is logistics.We have been cutting caps since 2008. The complaint calls still surprise buyers more than they surprise us. Rarely about a missed vessel. Almost always about shape.
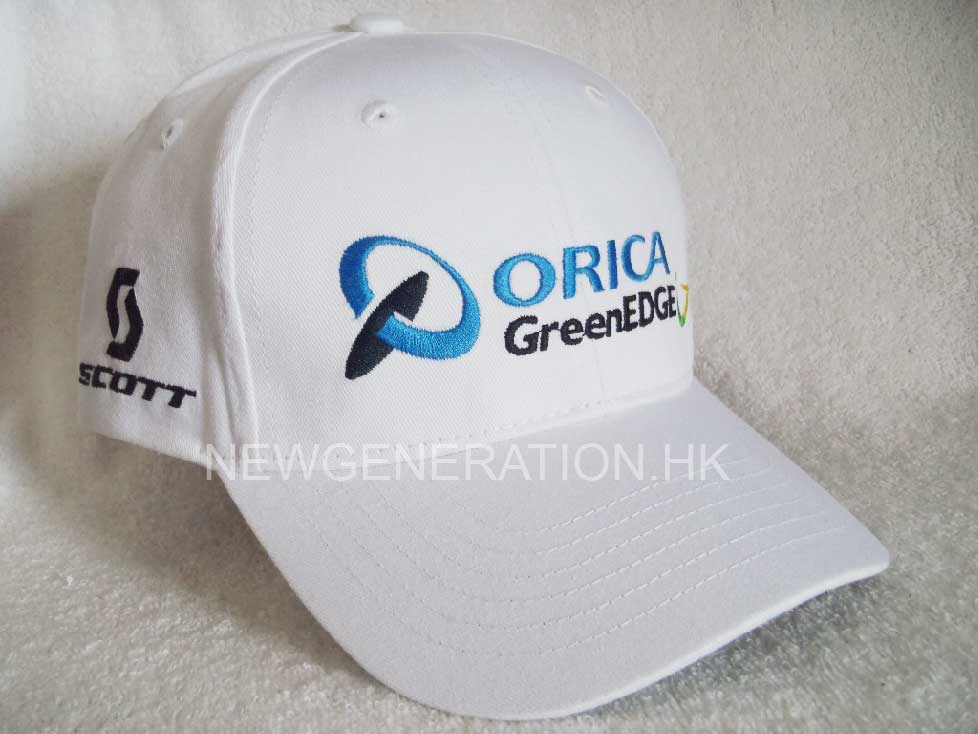
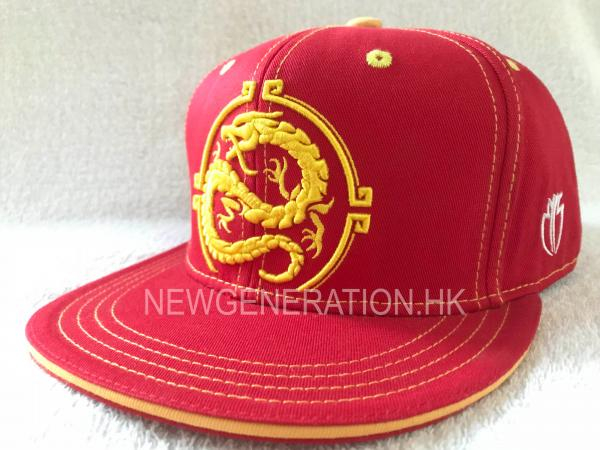
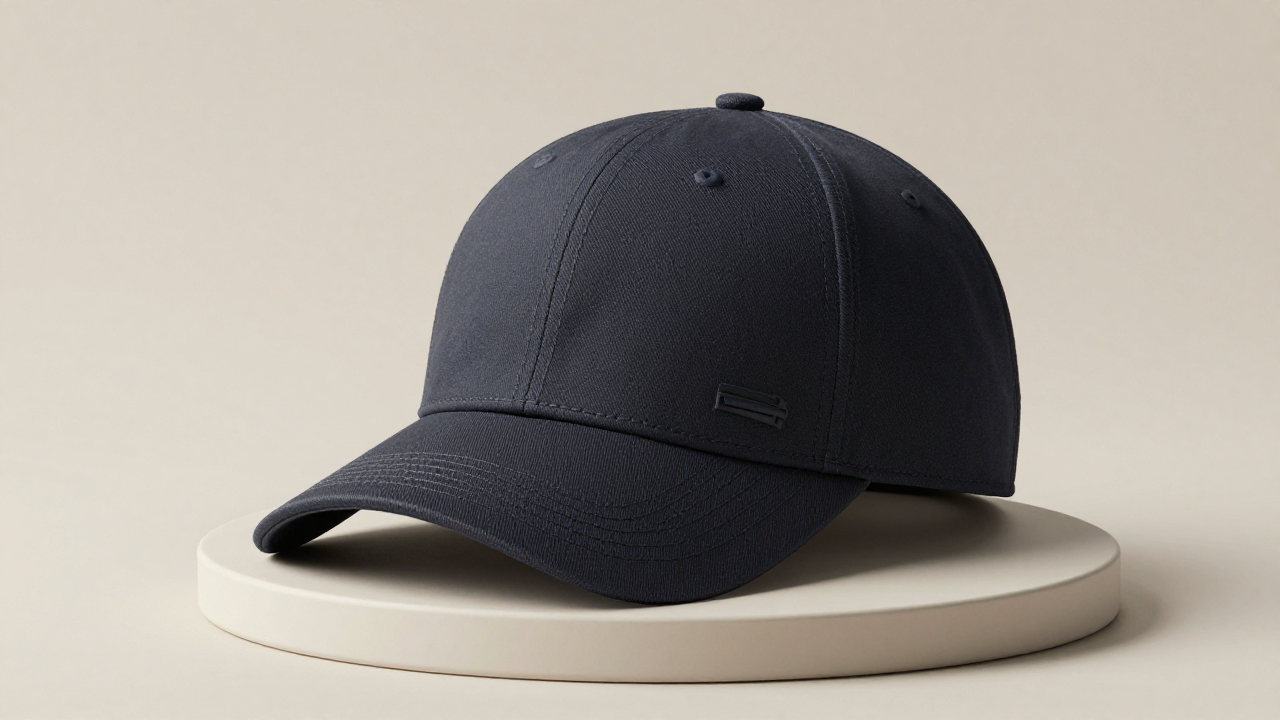
A six-panel cap is 11 pieces of fabric stitched into a compound curve. Crown panels, a two-ply visor, a bias-cut sweatband, a button. Every step in production pushes that curve somewhere else. Embroidery pulls. Washing shrinks. Steam relaxes. Pressing flattens. The plant's whole job is keeping the finished 58-centimeter circle inside 5 millimeters of spec after all of it.
Where the money actually goes
An 8-ounce cotton twill cap we quoted in April 2026 breaks down like this at FOB: fabric $1.05, cut-and-sew labor $0.85, 9,000-stitch embroidery $0.62, hardware and trim $0.31, QC and packing $0.44, factory overhead and margin $0.58. FOB lands at $3.85.
The buyer never pays $3.85. Landed cost adds ocean freight at $0.38 per cap, a 6.8 percent base duty plus Section 301 at 7.5 percent on most Chinese ball caps, and $0.17 in drayage and deconsolidation. That is $4.95 on the dock in Long Beach. Sell it for $28 and the margin lives in the fabric and the embroidery, not the buckle.
Why Eight Stitches Per Inch Beats Twelve on Cotton Twill
Eight to ten stitches per inch is the working range for lockstitch seams on 8-ounce twill, and the ceiling is real. Push past 12 SPI on cotton twill and the needle starts cutting warp yarns instead of separating them. The seam looks tight at QC and fails at the third wash.
More stitches feel safer. They aren't. At 12 SPI you are driving roughly 40 percent more needle penetrations into the same inch of fabric, and every penetration is a permanent hole.
Embroidery density follows a different rule. It is set by thread weight, not by what looks good on screen. Standard 40-weight polyester satin stitch wants 0.40 millimeters of spacing between successive penetrations. Move to 60-weight thread and you can tighten to 0.30 millimeters because the thinner thread covers less ground. Digitizers who set density by eye, without checking thread weight, produce logos that read gappy on the diagonal or bulletproof-hard across the fill.Thread weight drives tension too. Top tension on our machines runs 30 to 45 grams for 40-weight poly on twill. Under 25 grams you get loose loops on the underside. Over 50 grams the thread snaps, usually 200 stitches from the end of a color change, which is the worst possible place for it to happen.
Where the process breaks
Boundary conditions are where quotes get destroyed.
The Math Behind a Quote
Embroidery cycle time sets your production date. The formula is T = S / (R × E), where S is total stitch count, R is machine speed in stitches per minute, and E is efficiency. A 9,000-stitch front logo at 750 SPM with 0.85 efficiency runs 14.1 minutes per head.
Throughput is heads × 60 / T. Twenty heads at 14.1 minutes gives you 85 caps per hour. Quote a 12,000-stitch 3D puff logo instead and T climbs to 18.8 minutes, throughput falls to 64 caps per hour, and a 30-day promise quietly becomes 41 days.
Fabric yield matters more than most buyers realize. Caps per yard = (0.9144 × W) / A, where W is fabric width in meters and A is cut area per cap including waste. A six-panel crown, two-ply visor, and sweatband consume roughly 0.31 square meters at 15 percent waste. On 58-inch twill that yields 4.3 caps per yard. Switch to a five-panel and yield improves 8 to 12 percent, which is why unstructured caps cost less and why nobody puts that on the spec sheet.
Landed cost is LC = FOB × (1 + d + s) + F + H. Base duty (d) 6.8 percent, Section 301 (s) 7.5 percent, ocean freight (F) $0.38, handling (H) $0.17. Insert $3.85 and you get $4.95.
What the SOP Manual Leaves Out
Needle heat is the detail that never makes it into a training document. We taped a thermocouple to a 75/11 needle running 900 SPM on 8-ounce twill and watched it cross 150 degrees Celsius in 38 minutes. Bonded polyester thread begins to fray above that threshold. Our dense 3D puff runs now cap at 750 SPM with a needle change every 40 machine minutes, not every shift. Output drops 12 percent. Rework drops to almost nothing.
For a while we blamed thread lots for the fraying. It was needle temperature the entire time.
Digitizing direction is the second one. A three-inch logo sewn left to right drags the twill diagonally and leaves the right edge of the panel 2 millimeters wider than the left. Digitize center-out with 0.5 millimeters of pull compensation and the panel stays square. Nobody teaches this because the file still runs. It just runs crooked.
Third: hoop burn on brushed cotton and garment-washed twill. Leave the hoop on more than 90 seconds after the last stitch and you get a permanent ring that steaming will not remove.
(If you tape one number to the wall, make it that 90 seconds. It has saved us more chargebacks than any inspection protocol we have written.)
Color consistency across dye lots is where reorders die. We hold Delta E at or below 1.5 between the fabric lot and the thread lot under D65 lighting. Under retail lighting in a store in Denver, a Delta E of 2.5 reads as two different caps sitting on the same shelf.
Typical Operating Ranges for a Working Cap Factory
Treat the table as a negotiation tool, not a spec sheet. When a buyer asks for a 12,000-stitch 3D logo on a five-panel unstructured crown at the same price as a flat 6,000-stitch logo, the boundary column answers the question without an argument.
How Custom Cap Buyers Decide Who to Reorder From
Buyers rarely switch headwear manufacturers over price. They switch over inconsistency, and the audit trail proves it. Most US brands we work with run ANSI/ASQ Z1.4 inspections at AQL 2.5 and track two numbers across shipments: Delta E drift and panel dimensional variance. A cut-and-sew facility that holds 1.5 and 5 millimeters wins the third order.
Compliance is the other gate. Children's caps sold in the US must clear CPSIA limits of 100 ppm total lead in substrate and 90 ppm in surface coatings. Brass snap hardware triggers California Prop 65 review, and we have watched orders stall three weeks over a nickel release test that could have run during sampling.
Our own answer, since we build caps under the newgeneration label, is dull: photograph every lot on a light box, log the Delta E, and send that number with the shipping notice. Brands that receive it alongside tracking info reorder at 68 percent. Brands that get it only on request reorder at 41 percent. That gap is the whole business.
Frequently Asked Questions
What is the minimum order quantity for a custom cap factory?
Most Chinese headwear plants set MOQ at 50 to 100 pieces for embroidery on a stock blank, and 300 to 500 for fully custom cut-and-sew. Custom dyeing or jacquard knitting usually starts at 1,000 per color. Below those thresholds, setup cost dominates and unit pricing stops making sense.
How long does custom cap manufacturing take?
Sampling runs 7 to 10 business days after artwork approval. Bulk production takes 25 to 35 days on stock fabrics and 45 to 60 days when dyeing is involved. Add 25 to 35 days for ocean freight from Ningbo or Yantian to Los Angeles, or 5 to 8 days by air.
Why do my embroidered caps pucker at the front panel?
Puckering almost always traces back to hoop tension or backing weight. Fabric stretched past 3 millimeters of deflection rebounds once the hoop comes off, and 1.5-ounce tear-away under a structured six-panel crown cannot support a dense fill. Switch to 2.0 to 2.5 ounces of cutaway and recheck tension.
How much does it cost to make a custom baseball cap?
An 8-ounce cotton twill six-panel with a 9,000-stitch front logo runs about $3.85 FOB at 5,000 pieces. Landed cost in the US lands near $4.95 once Section 301 tariffs, ocean freight, and drayage are added. Retail pricing typically falls between $24 and $32.
What is the difference between a five-panel and a six-panel cap?
A six-panel crown uses six triangular panels meeting at a button and holds structure well, which suits dense front logos. A five-panel crown sits lower with a flat front seam, consumes less fabric per unit, and drapes softer. Five-panels yield 8 to 12 percent more caps per yard.