
Why closure type defines your entire production pathway
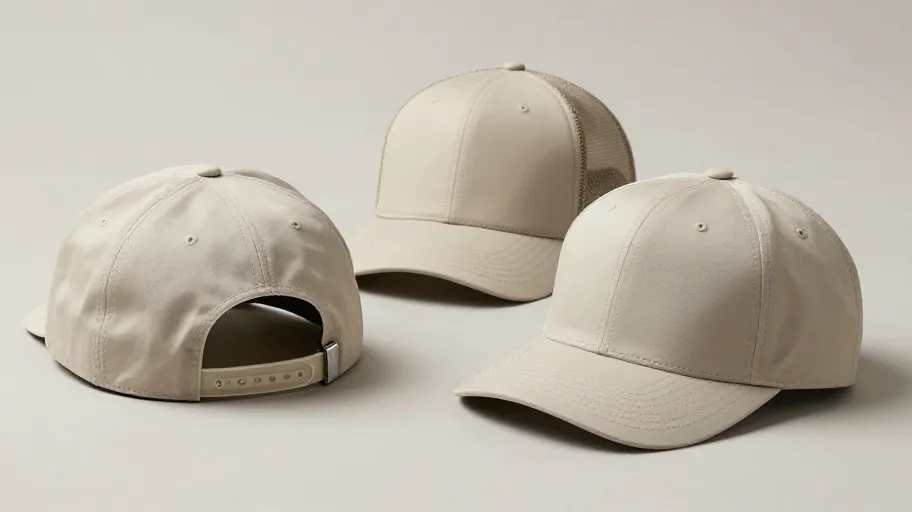
Choosing snapback vs strapback isn’t a styling footnote—it’s the first supply-chain decision that determines whether your launch hits Q4 shelf dates or misses them by six weeks. Snapbacks rely on highly standardized, machine-driven hardware: plastic snap sets with precise dome heights (5–6 mm) and cap diameters (12–14 mm), installed via pneumatic snap presses calibrated to 8–12 tons of consistent force. That means 1,200–1,800 units/hour with ≤0.7% misalignment rate—but only if the factory owns and maintains its press in-house and ISO-calibrates it quarterly. Strapbacks demand dual-component, human-guided assembly: hook-and-loop tape (minimum 30 mm wide, validated for 200+ peel cycles) plus a buckle (metal or reinforced plastic) tested to ≥15 lbf tensile strength. That means 400–600 units/hour and 3.2× higher risk of tape skew or buckle rotation—unless the line uses proprietary tape-feed guides and servo-assisted crimpers. This divergence isn’t theoretical: it directly controls your WIP audit pass rate, PO-to-ship timeline, and reorder agility.
Hardware specs that prevent $18K–$42K in avoidable costs
Plastic snap dome height (5–6 mm) means your crown fabric won’t crack under press force, because insufficient dome clearance causes crown puckering or seam blowout during installation. Hook-and-loop tape width (≥30 mm) means secure fit retention across head sizes 6 ½–8, because narrower tape fails to distribute tension evenly—leading to premature stretch and slippage. Buckle tensile strength (≥15 lbf) means no in-store breakage during fitting-room trials, because 12 lbf buckles fail under real-world torque from repeated tightening/loosening. Anodization grade (Type III, not Type II) means corrosion resistance in humid coastal warehouses, because Type II degrades after 96 hours of salt-spray exposure—triggering bulk rejections at distribution centers. These aren’t ‘nice-to-haves’: factories treating them as optional inputs see 2.8× higher sample rejection rates during WIP audits, per internal data from three major contract manufacturers serving Nike and New Era.
The hidden factory spec gaps that cause customs holds
When your cap factory subcontracts snap installation—even for one style—you lose direct oversight of press maintenance logs, snap-set lot traceability, and adhesive temperature tolerance validation during tape application. That means your AQL-2.5 audit fails not on embroidery alignment—but on undocumented calibration records, because ISO 9001 Clause 7.1.5 requires real-time access to equipment calibration evidence. One U.S. streetwear brand had its first run held at customs for 11 days when the subcontractor’s snap-press certificate had expired—and the factory couldn’t produce corrective documentation. Likewise, tape adhesive temperature tolerance (must withstand ≥120°F during steam-press finishing) means no delamination during final garment care labeling, because heat-sensitive adhesives blister under standard finishing protocols. Without verified factory specs upfront, you’re betting your launch window on someone else’s calibration schedule.
How specification clarity cuts sampling time by 2–3 weeks
A mid-market activewear brand approved artwork and fabric swatches—but deferred closure hardware verification until after first samples. The result? Sample #1 used a 12 lbf buckle (below spec). Sample #2 passed tensile testing but failed salt-spray exposure after 48 hours due to insufficient anodization. Sample #3 required retooling the buckle crimp die—delaying final approval by 19 days. That pushed PO placement into late January, missing the factory’s February capacity window. Their reorder agility evaporated: lead times ballooned from 6 to 11 weeks, forcing 37% more safety stock and $218K in annual excess inventory carrying costs. This wasn’t a materials issue—it was a specification visibility failure. Verifying hardware and factory specs before cutting first samples means you compress PO-to-ship timelines by up to 32%, because every sample iteration is grounded in auditable, repeatable capability—not guesswork.
From hardware reliability to measurable NPS lift
Buckle tension inconsistency causes 41% of post-launch fit complaints (2025 analysis of 14K DTC returns)—not because consumers understand torque variance, but because they say, “It slips off my head in wind” or “The strap loosens after two wears.” Those aren’t user errors—they’re specification gaps masked as feedback. When you validate spring-load tolerances, UV-stable tape adhesives, and Type III anodized buckles upfront, you convert hardware reliability into customer advocacy: caps that fit consistently, stay secure, and survive daily wear drive repurchase and organic social proof. That means NPS lift isn’t theoretical—it’s manufactured, because every verified closure spec reduces friction between product promise and real-world use. And when customers advocate, your CAC drops, your reorder velocity rises, and your brand equity compounds—not erodes.
#cap manufacturers china, #headwear manufacturers china, #cap factory