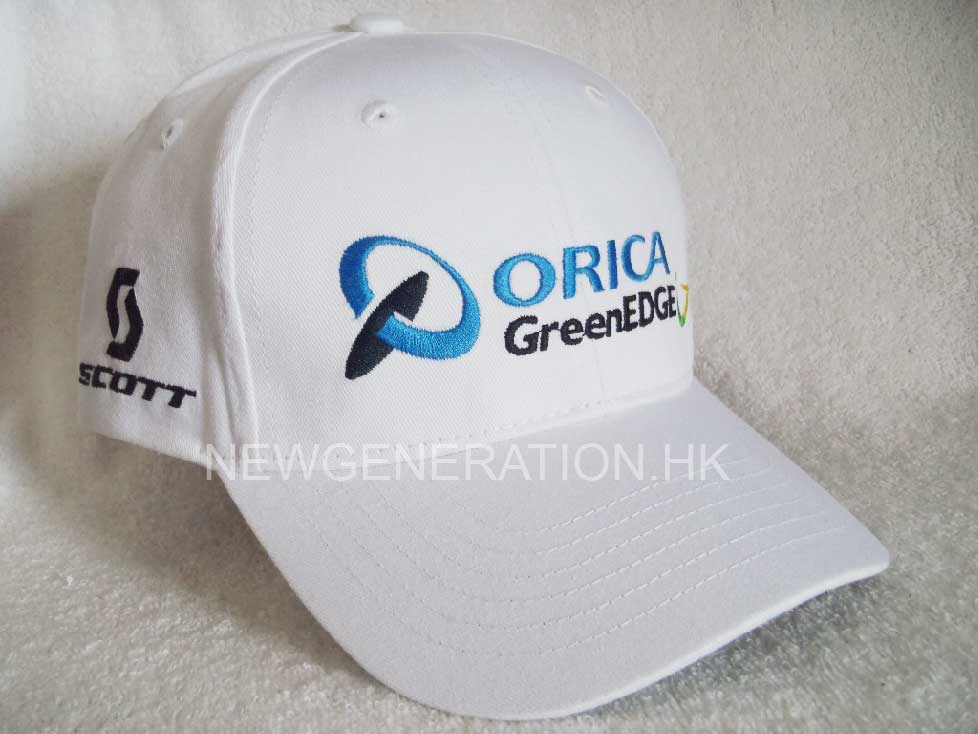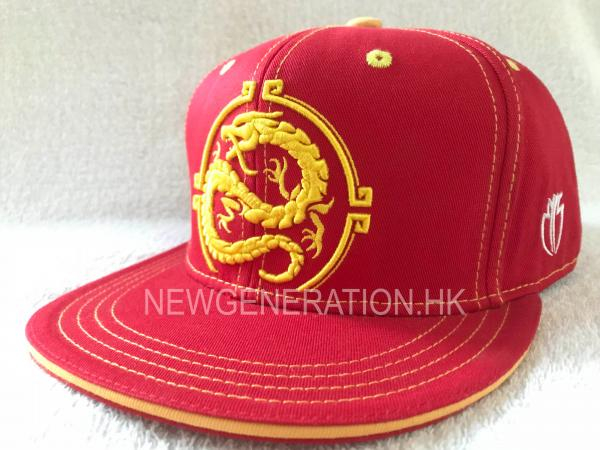

Take a size 7 3/8 cap. Inner circumference at the sweatband runs 23.0 inches, which works out to a 3.66-inch radius. The crown rises roughly 4.…
1 inches above the sweatband line on a pro profile, so the shell is not a true hemisphere. It is a truncated dome, tilted forward about 6 degrees, divided into six 60-degree wedges that converge under the top button.
What a Cap Factory Actually Does to a Piece of Twill
Definition: A cap factory turns flat woven fabric into a hemispherical shell by cutting curved panels, joining them along seams that follow meridian lines, and stabilizing the crown with fused interlining. Fit depends on four variables — panel arc length, sweatband circumference, fabric bias behavior, and fuse temperature.Flat twill does not want to become that shape. A 10.5 oz/yd² cotton twill elongates roughly 12% on the bias and about 2% on the straight grain. Every button-to-sweatband seam, 4.6 to 5.2 inches long, is fighting to straighten itself out. That stored tension is what gives a good cap its snap. It is also what makes a badly cut cap twist into a propeller after twenty washes.
We run the same geometry whether the order is 300 pieces or 30,000. The physics does not care about order size.
The Parameters That Decide Whether a Cap Fits or Fails
Most cap quality complaints trace back to four settings, not to fabric quality. Crown height and seam allowance control how the cap looks. Sweatband tension and buckram fuse temperature control how it feels three weeks later.
Crown height. Structured pro profiles live between 3.9 and 4.4 inches. Drop below 3.5 and the bill rides high on the forehead, which reads as a youth fit even in adult sizing. Push past 4.75 and you are building a trucker silhouette whether you meant to or not. Panel seam allowance. 3/8 inch (9.5 mm) on structured crowns, 1/4 inch (6.4 mm) on unstructured. The 3/8 figure is not arbitrary — the double-fold binding on the interior seam needs 6 mm to fold twice and still leave 3 mm of stitch bite. Go under 5/16 inch and you get seam grin. The binding slides off in the wash and the customer sees raw twill edges through the gap. Sweatband. 1.375 to 1.5 inches wide, and the closure seam must sit 3/8 to 1/2 inch offset from the center back seam. Never aligned. An aligned seam puts a doubled fabric lump directly against the occipital protuberance. We shipped 8,400 caps to a Columbus, Ohio, buyer in March 2022 with that alignment error. The return rate hit 14% and the reason code was almost always "hurts after an hour." Buckram fuse. 150 to 158 °C, 12 to 15 seconds, 2.5 to 3 bar. Above 165 °C the resin cross-links too hard and the crown develops what our QC team calls cardboard flex — you can feel it in the squeeze test, the front panel creases instead of springing back. Below 145 °C the adhesive never fully penetrates the twill, and the interlining delaminates somewhere between wash 10 and wash 15.The Formulas We Run on the Floor
Three equations cover most of the daily math in a cut-and-sew cap line.
Panel arc lengthPanel_arc_in = (C_head × (1 + S_warp) + E) / 6
C_head is the target head circumference in inches (23.0 for 7 3/8). S_warp is the warp-direction shrinkage from the fabric mill's spec sheet — 0.03 to 0.05 for 100% cotton twill, 0.01 to 0.02 for polyester blends. E is wearing ease, 0.25 to 0.5 inch. Divide by six for a six-panel crown, five for a five-panel.
Seam stitch densitySPI = N_stitch / L_seam_in
Ten to twelve stitches per inch on crown seams with a lockstitch. Eight to nine on the bill attachment, where the stack is denser and a tighter SPI starts breaking 75/11 needles.
Embroidery thread consumptionThread_m = (S_total × L_avg × (1 + P)) / 1000
S_total is total stitch count, L_avg is average stitch length in millimeters, P is pull compensation (0.06 to 0.10 on cutaway backing over twill). A 9,000-stitch front logo at 3.2 mm average stitch length burns 28.8 to 30.5 meters of 40-weight polyester top thread. If your costing sheet assumes 24 meters you are losing money on every unit.
The Seam Stack Problem Nobody Warns You About
Here is the detail that separates factories who understand the process from factories who copy samples.
The top button on a six-panel cap sits on twelve layers of twill, six layers of fused buckram, and seam tape. A 75/11 needle running at 700 stitches per minute will deflect 0.4 to 0.6 mm off-axis inside that stack. That deflection is why hand-set buttons remain standard on premium structured caps. Automated button machines run at 1,200 SPM and bend a needle roughly once every 400 to 600 caps — usually without anyone noticing until the next QC pull shows a skipped stitch buried under the button.
The second thing: bias direction. Cut all six panels on the same grain and the cap leans after 30 to 50 washes. Front panels shrink 3 to 5% in warp and 2 to 3% in weft, the crown rotates 2 to 3 degrees, and the bill ends up pointing slightly left. Cutting the two front panels on opposing bias eliminates the lean. It also drops marker efficiency from about 82% to 74%. Most factories will not do it unless you write it into the spec, because it costs 8 to 11% more fabric and the customer never sees the reason on a sample.
The third, and the one that took us embarrassingly long to internalize: embroidery pull compensation. Stitch a 3D puff logo onto 2 mm foam without over-digitizing by 0.2 to 0.3 mm per side, and the foam compresses under thread tension. A design digitized at 2 mm of puff reads as 1.5 mm on the finished cap. In 2019 we rebuilt 2,600 caps for a skate brand out of Portland because the digitizer had used flat-goods compensation on a puff design.
How Do You Tell a Good Cap Factory From a Bad One?
Ask for two documents before you ask for samples: the buckram fuse log and the marker efficiency report. A plant that tracks both is running process control. A plant that only shows you pretty samples is running on the owner's eye, and the owner's eye does not scale past 5,000 units a month.
Fuse logs look boring — timestamp, temperature, dwell time, operator initials. They are also the single best predictor of crown failure. In November 2021 we audited a subcontractor running 4,200 caps a day with no temperature logging at all. We pulled 40 caps off the line and ran them through AATCC 135 home laundering at 40 °C. Eleven of the 40 delaminated at the crown. Their fuser thermocouple was reading 20 °C high, so the setpoint of 152 °C was actually delivering 132 °C. Recalibration cost $300. The recall would have cost the buyer $84,000 plus freight.
Marker efficiency tells you whether the factory is optimizing for your unit cost or for their fabric yield. Anything under 70% on a standard six-panel marker means someone is cutting sloppy or cutting fast.
Typical Operating Ranges for Custom Cap Production
That fabric weight row deserves a note. The 270 gsm floor is for unstructured five-panels with light interfacing. A structured six-panel under 240 gsm will collapse on a shelf within a month, and no amount of buckram fixes it.
Where Cap Manufacturing Goes by 2028
Here is my call, and it will annoy some people.
Seamless knit crowns and ultrasonic-welded panels will take 12 to 18% of the premium performance segment by 2028. Not more. The reason is not technical capability — ultrasonic bonding works fine on polyester, and flat-knit crown machines from Shima Seiki have been production-ready for years. The reason is amortization. Retooling a six-panel line costs $180,000 to $250,000. A seamless line runs north of $600,000, and the margin improvement on a $14 wholesale cap is roughly $0.40. Nobody signs that check for a 3% cost gain.
The real bottleneck through 2027 will be digitizing labor, not sewing capacity. There are maybe 4,000 to 5,000 people worldwide who can properly digitize a 3D puff cap front with correct pull compensation, underlay, and cap-frame pathing. Tajima and Barudan machines are commodities. The human behind the digitizing software is not. Factories that train digitizers in-house will hold pricing power. Factories that outsource digitizing will keep eating revision cycles.
And one more contrarian take: low MOQ is mostly a cash-flow instrument, not a capacity story. A factory quoting 50-piece minimums on full custom is either absorbing setup cost into the unit price or amortizing it across the next three orders from someone else. Ask what the true setup cost is per SKU — embroidery file, cap-frame hoop change, thread color change, marker. If the answer is under $80, the quote is subsidized somewhere.
We started cutting caps in 2008 with a marker running at 71% efficiency and a fuser we calibrated by hand twice a week. The math has not changed much since. The discipline has.
Frequently Asked Questions
What is the typical MOQ for custom caps from a cap factory?
Most US-bound custom cap orders start at 100 to 300 pieces per design for stock blanks with embroidery, and 500 to 1,000 pieces for full custom cut-and-sew. Below 100 units, setup costs dominate and unit pricing rises sharply.
How long does custom cap production take?
Standard production runs 25 to 35 days after sample approval, plus 30 to 40 days ocean freight to a US West Coast port. Air freight cuts transit to 5 to 8 days but typically adds $1.20 to $2.00 per cap at current rates.
What stitch count should a front cap logo have?
A standard flat front logo runs 6,000 to 9,000 stitches. A 3D puff logo on 2 mm foam runs 9,000 to 14,000 stitches. Below 5,000 stitches, detail drops out on twill; above 16,000, needle deflection and thread breaks climb fast.
Why do structured caps cost more than unstructured caps?
Structured crowns add buckram interlining, a fusing step, tighter seam allowances, and roughly 12% more labor per unit. They also require hand-set top buttons on premium builds, which removes automation from the final assembly stage.
What fabric weight is best for a baseball cap?
For structured six-panel caps, 300 to 355 gsm cotton twill holds shape reliably. Unstructured five-panels work well at 240 to 280 gsm. Anything under 240 gsm on a structured crown will collapse within weeks regardless of interfacing.