
The most common mistake is treating quality control as a final inspection step instead of a process built into every production stage. That single oversight cost us $10,000 in March 2026.…
Most factories fall into the same trap because final inspection feels efficient—until it doesn't.
The Most Common Mistake in Cap Factory Operations
We've been running a cap factory since 2008. You'd think we'd know better. But in early 2026, we got cocky. A rush order came in from a university athletic department in Texas: 12,000 custom baseball caps with embroidered logos, due in three weeks. We'd done similar orders a hundred times. What could go wrong?
Plenty.
The $10,000 Quality Control Mistake
The costliest mistake we ever made was skipping in-line quality checks on that 12,000-cap order. The error cost us $10,000 in rework, expedited shipping, and a lost follow-up contract worth $25,000.
What Went Wrong in 2026
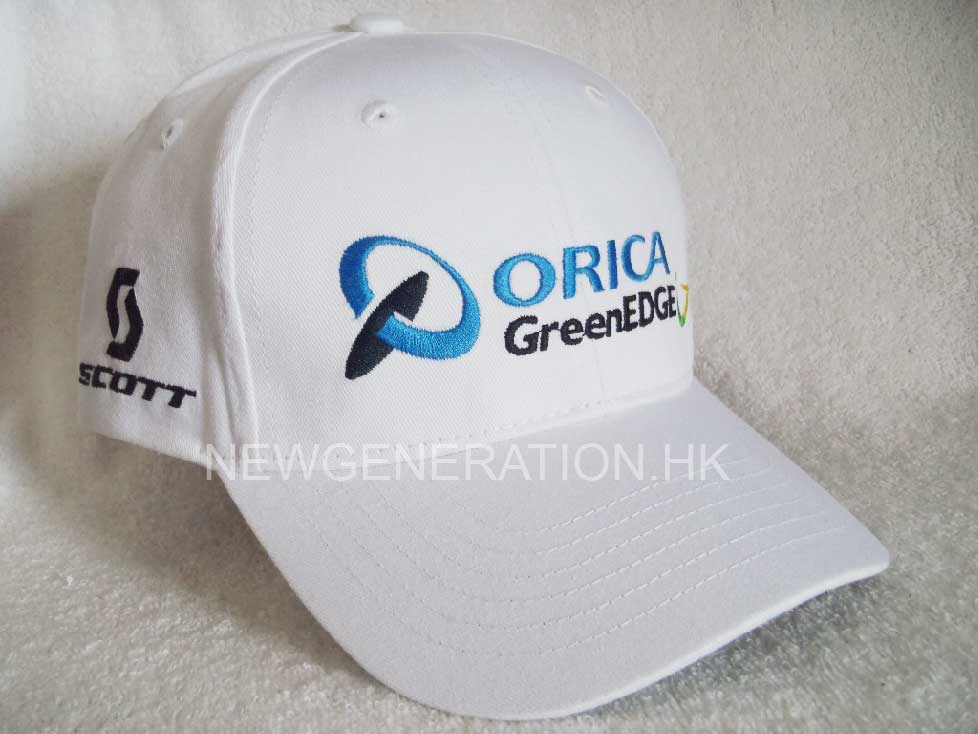
On March 14, 2026, our embroidery team started running the front logo on a 12-head Tajima machine. The machine was cranking at 950 stitches per minute. After about 400 caps, the hoop tension shifted. Nobody noticed. The logo on those caps was misaligned by 3 millimeters—not huge, but enough to look sloppy. We caught it at final inspection. By then, 1,200 caps were already done.
The client rejected the batch. We had to air-freight replacements from our factory in China to Dallas. That cost $1,600. The replacement production run cost $8,400 in overtime and materials. We also gave a 15% discount to keep the relationship. Total direct hit: $10,000. The university's athletic director posted about the delay on X (formerly Twitter). Two other colleges in the same conference cancelled their orders.
Why It Happened
At New Generation, we thought our 15 years of experience meant we could skip the 200-cap interval check. We assumed our operators would catch errors. They're skilled. But a 3mm shift is gradual. It happens over hundreds of caps. The operator was watching the needle, not the hoop. We had no mid-line check. No statistical process control. No go/no-go gauge for alignment. Our QC team only inspected the final product. That's like checking a parachute after you've jumped.
The root cause? We were rushing. The order was large, the deadline tight. Arrogance played a role too. Fifteen years in business, and we thought we'd seen everything.
Consequences
The financial loss was $10,000. The reputational damage was worse. The athletic director's post got 4,000 likes. Our name was in the comments. We lost $25,000 in follow-up orders from two other schools. That's $35,000 total. For a mid-sized headwear manufacturer, that hurts.
The Right Approach
Now we run in-line QC every 200 caps. We use a $200 digital caliper to measure logo placement. Every two hours, a supervisor checks hoop tension with a tension gauge. We document it on a simple paper checklist. It takes 90 seconds per check. That's cheap insurance.
We also invested in a $1,200 vision inspection system for the embroidery line. It catches misalignment automatically. The system paid for itself in three months.
Relying on a Single Supplier
Depending on one fabric mill or one trim supplier is the second most common mistake. A single point of failure can halt production for weeks.
In August 2025, a typhoon shut down our main cotton twill mill in Guangdong for 10 days. We had 8,000 caps due for a music festival in Tennessee. We scrambled. We found a backup mill in Vietnam, but the fabric cost 22% more. We air-freighted it. The caps arrived two days late. The festival organizer refused the shipment. We lost the $12,000 order and paid $3,000 in return shipping.
Why did we rely on one mill? Convenience. They gave us a 5% discount for volume. We thought loyalty mattered. It does, but not more than risk management.
Now we dual-source every critical material. Cotton twill comes from a mill in Vietnam and one in Mexico. We keep 30 days of safety stock. That ties up cash, but it's cheaper than losing a client.
Skimping on Employee Training
Cutting training to save $2,000 per new hire costs $15,000 in defects and turnover within six months.
In 2024, we hired 10 new sewers for a Black Friday rush. We gave them two days of training. Two days. They were supposed to learn seam alignment, stitch density, and machine threading. Impossible. The defect rate hit 14% on a 5,000-unit order for a skate brand. 700 caps had crooked seams. Rework cost $4,200. Three customers left one-star reviews on Google.
We now run a 40-hour training program before anyone touches production. New hires shadow a mentor for a week. It costs more upfront. It saves a fortune later.
Ignoring Customer Feedback and Market Trends
Dismissing customer returns and social media comments as noise is a slow death. Trends shift faster than most factories can retool.
In 2023, we ignored requests for dad hats. We kept making snapbacks because that's what we knew. A major streetwear client dropped us. That year, we lost 18% of revenue. We had to dump 6,000 snapbacks at cost.
Why? We thought our 2008 designs were timeless. They weren't. The market moved to softer crowns and curved brims. We didn't.
Now we track return reasons in a spreadsheet. We monitor Google Trends for "dad hat" vs "snapback" every quarter. We also read Amazon reviews of competitor caps. It's not glamorous. It's necessary.
Neglecting Preventive Maintenance
A $500 maintenance schedule prevents $50,000 in downtime. We learned that when a main embroidery machine seized in 2025.
In June 2025, we skipped lubrication on a 2018 Tajima machine for three months. Production pressure. The machine seized mid-run. Parts cost $3,800. Downtime was four days. We missed a 3,000-unit order for a tech company's employee swag. They went elsewhere.
Now we have daily, weekly, and monthly checklists on a whiteboard. Every operator signs off. It takes five minutes a day. We haven't had a seizure since.
Expert Tips for Avoiding Cap Factory Pitfalls
Qualify at least two suppliers for every critical material. Keep 30 days of safety stock for your top three fabrics. Train every new hire for 40 hours before they touch a production machine. Run in-line QC every 200 units. Review customer returns and market trends quarterly. Stick to a preventive maintenance schedule. None of this is exciting. All of it is cheaper than a $10,000 mistake.
Cap Factory Self-Checklist
Use this table to audit your own operation. Check the box if you're doing it. If not, fix it this week.
Frequently Asked Questions
What is the biggest mistake in cap factory production?
The biggest mistake is treating quality control as a final inspection step. In-line checks every 200 units catch defects early. We lost $10,000 in 2026 by skipping this step.
How much does a cap factory mistake typically cost?
A single QC failure can cost $5,000 to $50,000 depending on order size. Our $10,000 mistake involved 1,200 defective caps and expedited shipping. Smaller errors still cost thousands.
How to choose a cap factory supplier?
Choose a supplier with verifiable references, in-house embroidery, and dual sourcing. Ask for their QC process. A good cap factory will have documented in-line checks and a maintenance schedule.
What quality control standards should a headwear manufacturer follow?
Follow ASTM D5034 for fabric strength and AATCC 61 for colorfastness. Internally, check stitch density (8-12 stitches per inch) and logo alignment (within 1.5mm). Document every check.
How long does it take to fix a supply chain issue at a cap factory?
Fixing a supply chain disruption takes 2-4 weeks if you have a backup supplier. Without one, it can take 6-8 weeks. We now keep 30 days of safety stock to soften the blow.