
That one sentence explains why two factories quoting the same cap at the same price produce wildly different field-return rates six months later.
What U.S. Buyers Actually Mean by Cap Manufacturers in 2026
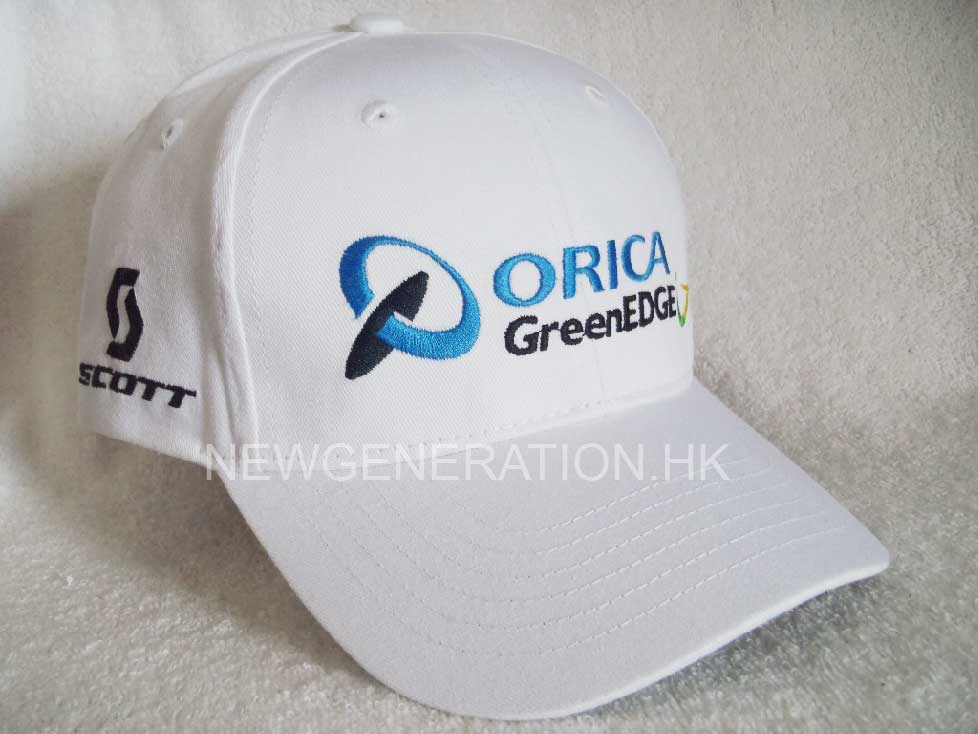
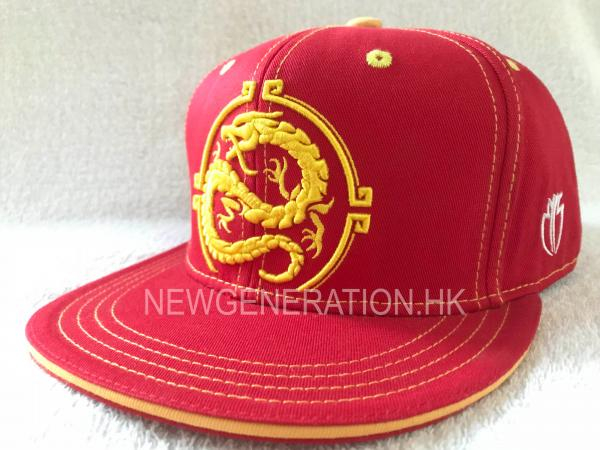
Cap manufacturing quality is the controlled balance of material flow, mold design, process stability, and inspection capability. Defect reduction happens fastest when variation is removed at the source instead of sorted out at the end.The word "cap" carries three different meanings inside U.S. purchasing teams, and that ambiguity burns a week off every program. A beverage closure buyer means a 28mm PCO threaded cap molded on a 48-cavity hot runner tool. A promotional products buyer means a decorated six-panel cap pulled from a blank catalog. A brand buyer means a custom cut-and-sew headwear program with a proprietary crown pattern, digitized embroidery files, and a wash spec.
All three land on the same search results. Between January and June 2025, about one in five RFQs that reached our sales inbox asked for 28mm tamper-evident closures. We make headwear. Each of those emails cost the buyer roughly a week of quoting back-and-forth.
Settle it in the first message: product category, annual volume, target landed cost, and whether tooling already exists.
The defect-reduction loop
Three stages decide your defect rate, and they run in sequence.
Design for manufacturability sets the ceiling. A closure gate placed 4mm off the weld line will leak at 40 psi no matter how the press is tuned. A cap crown drafted at 1.5° instead of 3° will fight you for the life of the tool.
Process control holds the ceiling. Mold temperature drifting 2°C across a shift moves PP shrinkage about 0.05%, enough to push removal torque outside an 8-16 in-lb window on a 28mm closure.
Inline inspection catches what escaped. If inspection is your main defense, you already lost. Sorting a bad lot costs 20-60 times more than scrapping the same parts at the press.
Why Cap Quality Comes Down to Physics, Not Promises
Every cap defect traces back to how polymer or fabric behaved at a specific temperature, pressure, and time. Parameters set the outcome. A factory that can show cavity pressure curves beats a factory with a nicer brochure, every time.From first principles to production settings
Start with melt temperature. Polypropylene copolymer for closures runs 210-250°C (410-482°F). Below 210°C the melt is too viscous to fill a 0.9mm tamper band before it freezes. Above 250°C you start degrading the polymer, and the degraded layer weakens the sealing surface without ever showing up on a visual check.
Cooling is where the clock lives. Cooling time scales with the square of wall thickness:
t ≈ h² / (π² × α)where t is cooling time in seconds, h is the thickest wall in millimeters, and α is thermal diffusivity (roughly 0.09-0.11 mm²/s for PP). Drop wall thickness from 1.6mm to 1.0mm and cooling time falls about 60%. That is the only lever that actually moves cycle time on thin-wall closures, which is why the argument over "faster machines" wastes everyone's afternoon. Cooling typically eats 60-70% of the total cycle.
Shrinkage is not one number. PP shrinks 1.0-2.5%, and it shrinks differently along the flow direction than across it. Tool makers compensate with a shrink factor, but that factor is only valid inside a specific mold temperature band. Move mold temperature 15°C and the compensation is wrong.
Where caps actually fail
Boundary conditions matter more than setpoints. A cap turns weak when two flow fronts meet cold and never knit. It warps when mold temperature is uneven across core and cavity. It leaks when hold pressure drops before the gate seals. It goes inconsistent when regrind content creeps past 15% and nobody updates the spec sheet.
What Best-in-Class Cap Manufacturers Measure Every Shift
High-performance cap manufacturers log cavity pressure, mold temperature, cycle time, shot weight, and torque every shift. A shift that drifts 3°F is the shift that ships the defect. Quarterly audits catch it after the fact.The formulas that explain your defect economics
Yield: Y = G / S × 100, where G is good caps packed and S is caps started (shots × cavities). Escape rate: E = (D / G) × 1,000,000, where D is defects found after your receiving dock and G is good units shipped. Rolled throughput yield: RTY = Y1 × Y2 × Y3 × … × Yn. Five stations each running 98% gives you 90.4% overall. That gap between 98% and 90% is where most quotes quietly go wrong. Cost of poor quality per 1,000 caps: CPQ = (R × Cm) + (E ÷ 1,000,000 × 1,000 × Cf). R is rejects per 1,000, Cm is material plus machine cost per cap (about $0.04-$0.09 for a molded closure), and Cf is field failure cost. In U.S. retail programs, Cf commonly lands between $3 and $8 once freight, credit, chargebacks, and the account review are counted. Clamp force: CF = (A × P) ÷ 2,000, where A is projected area in square inches and P is cavity pressure in psi. A 48-cavity 28mm tool has roughly 46 in² of projected area. At 5,000 psi that is 115 tons, which is why those tools sit on 150-250 ton presses.Reference ranges you can paste into an RFQ
Why Venting and Gate Balance Create Invisible Defects
Vent depth and gate balance decide whether a cap passes inspection today and fails in the field 90 days from now. Neither number appears on a standard datasheet, and most QC teams never measure them.The shop-floor problem nobody writes down
Vents sit on the parting line at 0.0005-0.0010 inches deep with a land length of 1.5-3mm. At the low end that is thinner than a human hair. Run 200,000 shots of PP with mold release sprayed twice a shift, and the vents load up with gas deposits.
Fill pressure then has nowhere to go. You get short shots on the last cavities, burn marks where trapped gas ignites, flash on the overpacked cavities, and a weld line on the tamper band that knits at maybe 60% strength. All of it passes a visual check.
Gate balance is the quieter killer. In a 48-cavity hot runner tool, if cavity 3 fills 6% faster than cavity 41, cavity 3 overpacks while cavity 41 underfills. Both parts measure inside print. They behave differently under torque. A capping line running 400 bottles a minute finds that difference in about four hours.
In September 2023 we rebuilt a 48-cavity closure tool in our Ningbo shop after a U.S. buyer reported torque failures on a snapback hardware program. Torque spread across cavities measured 4.2 in-lb. Re-cutting vents and rebalancing gates brought it to 1.1 in-lb, and not one process setpoint changed.
The headwear version of the same physics
Six-head embroidery runs identical mechanics. The heads share a pantograph, so if tension on head 2 runs tighter than head 5, stitch registration drifts 0.5-1.2mm over an eight-hour shift. You see it as a logo sitting 1mm off center on one cap out of nine, and never on the sample you approved.
We hold that drift with per-head tension logs every four hours plus a wash test to AATCC 135 on each dye lot. Cotton twill moves 3-5% on the first home wash. A 65/35 poly-cotton blend moves 1-2%. Cut the crown for the wrong one and the cap that fit in the sample room will not fit after the customer's first laundry cycle.
How experienced teams find root cause first
Good teams run a cavity pressure study before touching a setpoint. They pull a shot, weigh every cavity, and compare. Weight spread above 1.5% means gate imbalance, not a process problem. Standard QC teams do the reverse: they adjust hold pressure, then temperature, then cycle time, and burn eight hours chasing a tooling issue with settings.
How to Evaluate Cap Manufacturers Before You Place an Order
Ask for process data, tooling ownership documents, and a test result from the actual production tool. A supplier who cannot deliver all three within 48 hours is usually a trading company reselling someone else's floor.The due-diligence checklist
Certifications carry real weight in U.S. retail: ISO 9001:2015 for process discipline, WRAP or amfori BSCI for labor, Sedex SMETA for social audits, CPSIA and Prop 65 test reports if the headwear touches children's channels. Get certificate numbers with expiry dates, then verify them on the issuing body's site.
Then work the operational items: tooling capability (in-house or subcontracted), pre-production sampling off the real tool rather than a similar cap, quoted lead time with the port of loading named, MOQ, and lot traceability tying a finished cap back to machine, shift, resin batch, and pack date.
For custom headwear, expect MOQ of 300-500 pieces at most Chinese factories, 7-10 days for a photo sample, and 25-35 days for bulk. Ocean freight to Los Angeles or Long Beach adds another 30-35 days. Any program that has to land before Black Friday needs a sample cut by June.
If you need under 500 units with a three-week turnaround, screen domestic decorators first. If you need 5,000+ units with a proprietary crown pattern, verify tooling ownership before anything else. If the product touches kids' channels, ask for the CPSIA report before you approve the sample.
What an unknown supplier can do to prove itself
A factory with 17 years of production history still gets treated as unknown until it publishes evidence. The ones that win U.S. business film a walkthrough with time stamps and machine tags visible, export cavity pressure data on request, pay for third-party inspection through SGS or Bureau Veritas when the buyer asks, and name two reference customers willing to take a call. A supplier who hesitates on the reference call is the one to worry about.
What Buyers Get Wrong When Sourcing Cap Manufacturers
The most expensive mistake in cap sourcing is choosing on unit price and paying for it in field returns, chargebacks, and re-runs. The second most expensive is assuming the mold belongs to whoever paid the invoice.Buying on price alone and ignoring defect economics
Two quotes land: $0.88 and $1.00 per cap. That 12-cent gap looks like $6,000 on a 50,000-unit order. Now run the escape math. A 1% escape rate at a $6 field cost is $3,000 in returns, before freight and the account review meeting. Add a 2% higher scrap rate and the cheap quote is behind before the container clears the port.
Tooling ownership, resin compatibility, post-production inspection
Tooling is what buyers forget until they want to leave. Get a mold ownership certificate in your company's name, a mold life log showing shot counts, and photos of your part number stamped on the plate. Confirm the tool's physical location in writing.
Resin compatibility is the second trap. If your spec calls for 30 MFI polypropylene copolymer and the factory substitutes a 40 MFI "equivalent," the cap fills easier and impacts weaker. Nothing on the packing list tells you.
Post-production inspection should run on ANSI/ASQ Z1.4 sampling. "We check everything" is not a sampling plan. Ask for the AQL level and the inspection report format before the first shipment leaves.
Frequently Asked Questions
What is the difference between a cap manufacturer and a closure supplier?
A cap manufacturer produces headwear or molded plastic caps; a closure supplier makes bottle and jar closures. The two share injection molding physics and nothing else, since the molds, standards, and buyers differ. U.S. buyers searching "cap manufacturers" usually mean headwear factories, so state your product category in the first email.
What process data should a serious cap manufacturer share on request?
Cavity pressure curves, mold temperature logs, cycle time records, shot weight spread across cavities, and torque or wash-test results by lot. A supplier running cavity pressure sensors can export this within 48 hours. If the answer is a photograph of a machine display, the factory is not collecting data at all.
How long does custom cap production take from sample approval?
Typical timeline runs 7-10 days for a photo sample, 5-7 days for a pre-production sample, then 25-35 days of bulk production, plus 30-35 days ocean freight to Los Angeles or Long Beach. From October through Chinese New Year, add 10-14 days because embroidery and dyeing capacity tightens across Guangdong and Zhejiang.
How much does it cost to switch cap manufacturers mid-program?
Budget 8-15% of annual program value. Costs include new digitizing files, a second pre-production sample round, mold transfer or remanufacture, and 4-8 weeks of parallel running. Switching is cheapest when you own the tooling and the digitizing files before the first order ships.
How do I verify tooling ownership before placing an order?
Request a mold ownership certificate naming your company, a mold life log showing shot counts, and photos of the mold plate stamped with your part number. Then confirm the tool's physical location in writing. Buyers who skip this step have paid twice for the same mold, sometimes at the same factory.