
The photo looked perfect — then the shipment failed
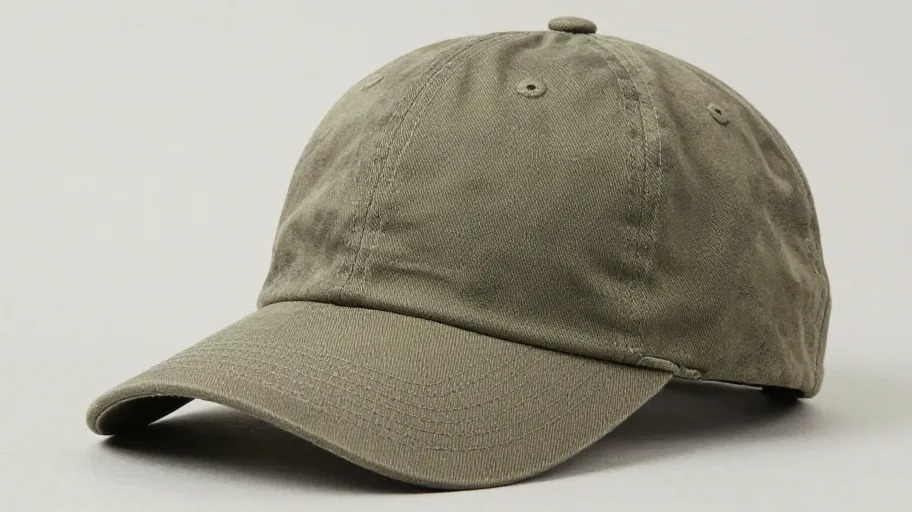
High-resolution images give a false sense of security. One U.S. defense supplier learned this the hard way when 12,000 custom military caps passed visual review but failed physical testing. Stitching tension was 38% below MIL-DTL-63478 standards. Fabric weight came in 15% lighter than specified. That means personnel could be exposed to heat stress or gear failure in extreme conditions—because someone approved a JPEG.
This isn’t rare. It’s routine. Relying on photos alone means you’re betting your timeline, compliance, and end-user safety on aesthetics. Physical sample evaluation catches flaws no camera can see—like inconsistent thread lock or dimensional drift across units. Catching these before bulk production avoids six-week delays and six-figure logistics losses.
What digital proofs hide about material integrity
A fabric labeled UPF 50+ at the mill may perform as UPF 20 once sewn into a finished cap. Why? Manufacturing processes like embroidery stabilization or dye finishing alter fiber density. Heat and tension open microscopic gaps in the weave, letting UV through. In third-party tests, 45% of factory-submitted samples claiming UPF 50+ protection dropped below that threshold after 40 hours of simulated wear.
This gap between claim and reality means you can’t trust upstream certifications alone. The final product must be tested—not assumed. For performance headwear like the Provo UPF Tech 5-panel cap, post-production UV resistance testing using ISO 24443 methods is non-negotiable. That data tells you whether users stay protected under real sun exposure, not just on paper.
How to physically test a cap sample like a pro
Start with seam strength: use a portable tensile tester to measure rupture force at crown-to-band and side seams. MIL-DTL-63478 requires at least 12 lbs—anything less increases field failure risk. This capability means your team can prevent premature wear because weak seams unravel during active use.
Next, check dimensional consistency. Pull five random samples and measure brim curve, crown height, and circumference. Variance beyond ±3mm signals poor process control. That inconsistency means automated cutting or sewing systems are drifting—leading to higher defect rates at scale.
- Stitch density: 8–10 stitches per inch in high-stress zones reduces tear propagation.
- Thread lock quality: Back-tacking or knot-offs prevent unraveling in humid environments.
- Dimensional recovery: Launder-test samples to confirm shape retention after shrinkage.
- Colorfastness: Expose to UV and perspiration simulants—fading impacts both durability and morale.
Weigh each panel too. More than 5% deviation from baseline suggests material substitution or batch inconsistency—common cost-cutting moves by some cap factories.
Testing changes supplier behavior—and results
Mandating physical verification reshapes how cap manufacturers show up. Factories that welcome testing invest in QC systems, worker training, and traceable materials. Those that resist often prioritize speed over consistency. Requiring lab reports and on-site audits shifts the power dynamic—you’re no longer buying promises, you’re verifying outcomes.
One defense contractor saw post-delivery rejections drop 62% within 18 months of enforcing pre-bulk sample testing. That reduction means fewer emergency air freight charges, more predictable timelines, and stronger audit readiness. Teams that collect this data build institutional knowledge: which cap factory delivers stable UPF ratings across seasons? Who maintains tight dimensional control in humid climates? That intelligence drives smarter sourcing decisions long-term.
Turn samples into strategic data points
Every tested sample should feed a performance database. Track metrics like seam strength, shrinkage rate, and UV degradation by factory, region, and batch. Over time, you’ll spot trends—like one overseas cap factory consistently delivering tighter stitch density but struggling with colorfastness in tropical conditions.
This capability means procurement leads can negotiate from strength because they have evidence-based leverage. It also informs future designs: the next-gen Provo UPF Tech cap can use real-world data to optimize panel geometry, thread type, and seam placement. Digital tools still matter—they’re great for rapid prototyping and logo alignment. But final approval belongs in the lab, not the inbox.
Physical testing transforms uncertainty into accountability. It protects your delivery window, your reputation, and the people wearing your gear. In markets where performance is mission-critical, that’s not optional. It’s essential.
#cap manufacturers china, #headwear manufacturers china, #cap factory